
Custom Security Cages & Wire Partition Enclosures: Get a Quote Today
MH-USA provides turnkey security solutions, from DEA-compliant pharmaceutical cages to high-security server room enclosures. Our experts offer free layouts and professional installation using top brands like SpaceGuard and BeastWire to ensure your facility meets all safety and compliance standards.
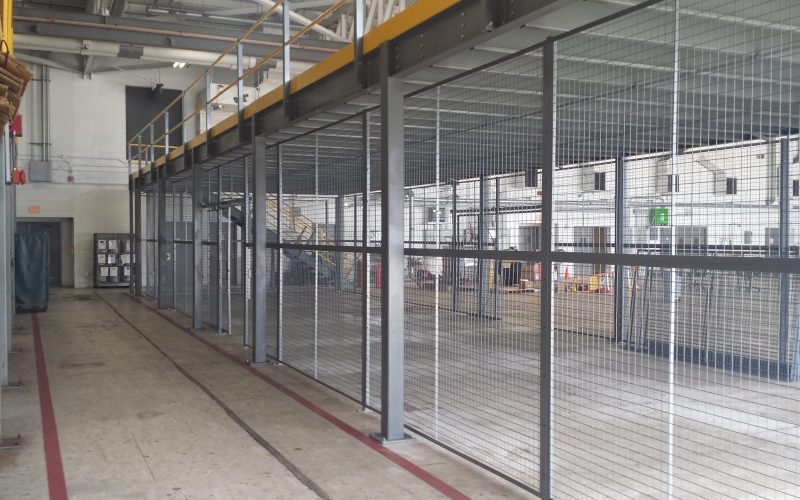
Comprehensive Security Cage Overview and Key Engineering Features
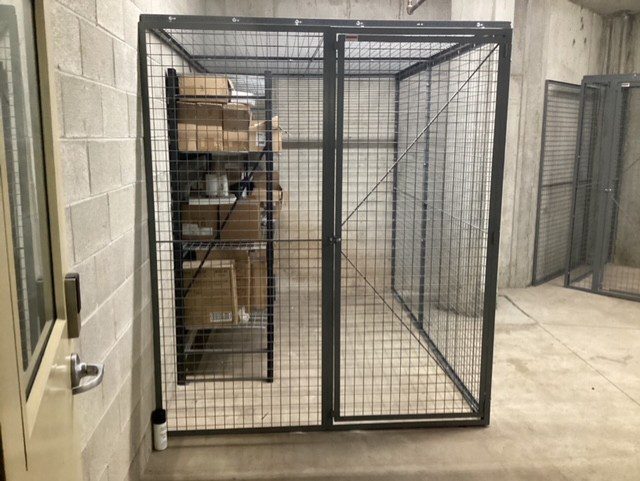
At Material Handling USA, our security cages and wire partitions represent the gold standard in industrial asset protection and spatial organization. These systems are engineered to provide a robust physical barrier while maintaining maximum visibility and airflow within your facility. Unlike traditional drywall or masonry partitions, our wire enclosures are modular by design, allowing for rapid reconfiguration as your warehouse or laboratory needs evolve.
We partner with industry-leading manufacturers like SpaceGuard and BeastWire to ensure that every panel, post, and gate meets rigorous structural standards. Our standard configurations typically feature 10-gauge wire woven into a 2-inch diamond mesh or welded into a 2-inch square pattern, providing a formidable deterrent against unauthorized access and internal shrinkage.
Tamper-Proof Frames and Hardware
The architectural integrity of our security cages is defined by their heavy-duty steel frames and secure hardware. Each system is designed to be tamper-proof, with assembly hardware that is only accessible from the inside of the enclosure, preventing intruders from dismantling the panels from the exterior.
We offer a variety of frame options, including cold-rolled steel channels and structural angle frames, which provide the necessary rigidity for high-traffic industrial environments. Whether you are securing high-value electronics, hazardous materials, or sensitive documents, our systems provide a professional, clean aesthetic that integrates seamlessly with existing warehouse racking and shelving systems from brands like Borroughs and Jaken.
Free Layout Service and Custom Sizing
Customization is at the heart of our product offering. Every quote from MH-USA includes a free layout service where our specialists analyze your floor plan to optimize space utilization. We consider critical factors such as ceiling height, floor obstructions, and the specific dimensions of the items being stored.
Our features extend beyond simple walls; we offer integrated ceiling panels for full six-sided protection, ensuring that assets are secure even in facilities with high ceilings or open rafters. This comprehensive approach to design ensures that your security cage is not just a fence, but a fully integrated security solution tailored to your facility’s unique footprint.
Visibility, Lighting, and Sprinkler Compatibility
Furthermore, our security cages are designed with safety and compliance in mind. The open-mesh design ensures that your facility’s existing lighting, HVAC, and fire suppression systems remain effective. Fire marshals often prefer wire partitions over solid walls because they allow sprinkler water to penetrate the enclosure, potentially lowering insurance premiums and ensuring your building remains up to code. By choosing MH-USA, you are investing in a high-quality, durable product that balances the need for high-level security with the practical requirements of a functioning industrial or commercial workspace.
Specialized Configurations: From DEA Cages to Server Enclosures

MH-USA provides an extensive array of wire partition configurations designed to meet the diverse needs of modern industry. One of our most sought-after solutions is the DEA-compliant pharmaceutical cage. These enclosures are specifically engineered to meet Title 21 CFR Part 1301.72 regulations for the storage of Schedule III through V controlled substances.
These cages feature panels mounted flush to the floor, heavy-duty self-closing and self-locking doors, and wire mesh ceilings. By utilizing high-security components from manufacturers like SpaceGuard, we ensure that pharmaceutical distributors and healthcare facilities remain in full compliance with federal mandates while protecting sensitive inventory.
Server and Colocation Cages
For data centers and IT departments, we offer specialized server enclosures and colocation cages. These systems are designed to protect sensitive rack equipment while allowing for the massive airflow required to prevent hardware overheating. We can integrate these cages with electronic strike locks, biometric scanners, or keypad entry systems to provide a digital audit trail of who accesses the server room.
Additionally, our driver cages or “man traps” are an essential safety configuration for logistics hubs. These small, secure enclosures are installed around warehouse entry doors, confining delivery drivers and visitors to a designated area while preventing them from wandering onto the warehouse floor where heavy machinery like forklifts are in operation.
Tool Cribs and MRO Lockers
Beyond standard security, we offer specialized tool cribs and maintenance lockers that utilize components from brands like Metro and Aurora. These configurations are ideal for organizing high-value tools, MRO supplies, and equipment that require restricted access.
We offer a variety of gate options to suit these spaces, including sliding doors that save floor space, traditional hinge doors for smaller openings, and Dutch doors with service counters for issuing tools or parts. For facilities requiring extreme durability, our welded wire partitions provide a rigid, non-raveling alternative to woven wire, making them ideal for heavy industrial applications where the cage might be subject to impact from carts or pallets.
Hybrid Wire and Modular Building Layouts
Finally, our modular building integration allows us to combine wire partitions with Panel Built structures to create hybrid workspaces. This might include a secure wire-enclosed storage area located beneath a mezzanine or adjacent to a modular office. We also provide floor-to-ceiling partitions that can reach heights of over 30 feet using stacked panels and reinforced support posts.
No matter the complexity of the layout, our team can configure a system that includes specialized cut-outs for conveyors, pipes, or electrical conduits, ensuring that the security perimeter remains intact while allowing for necessary facility utilities to pass through unobstructed.
Applications and Industries: Protecting Assets Across Every Sector
MH-USA security cages are indispensable across a wide spectrum of industries. Every application below is a system we routinely design and install — find the environment closest to yours.
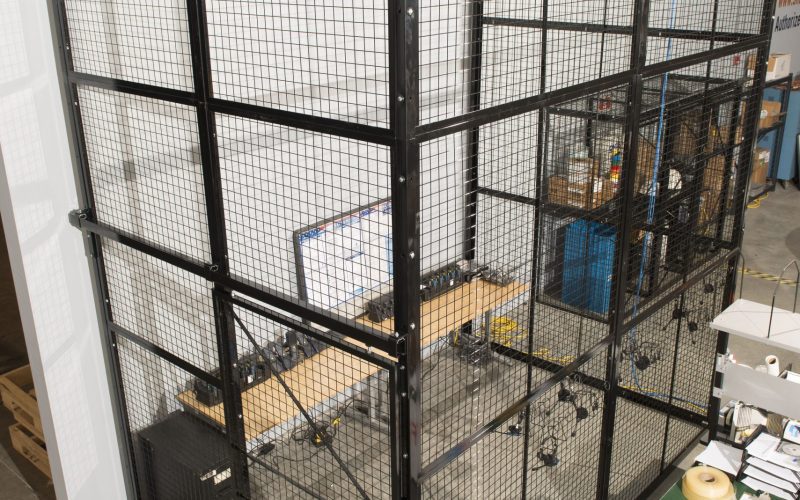
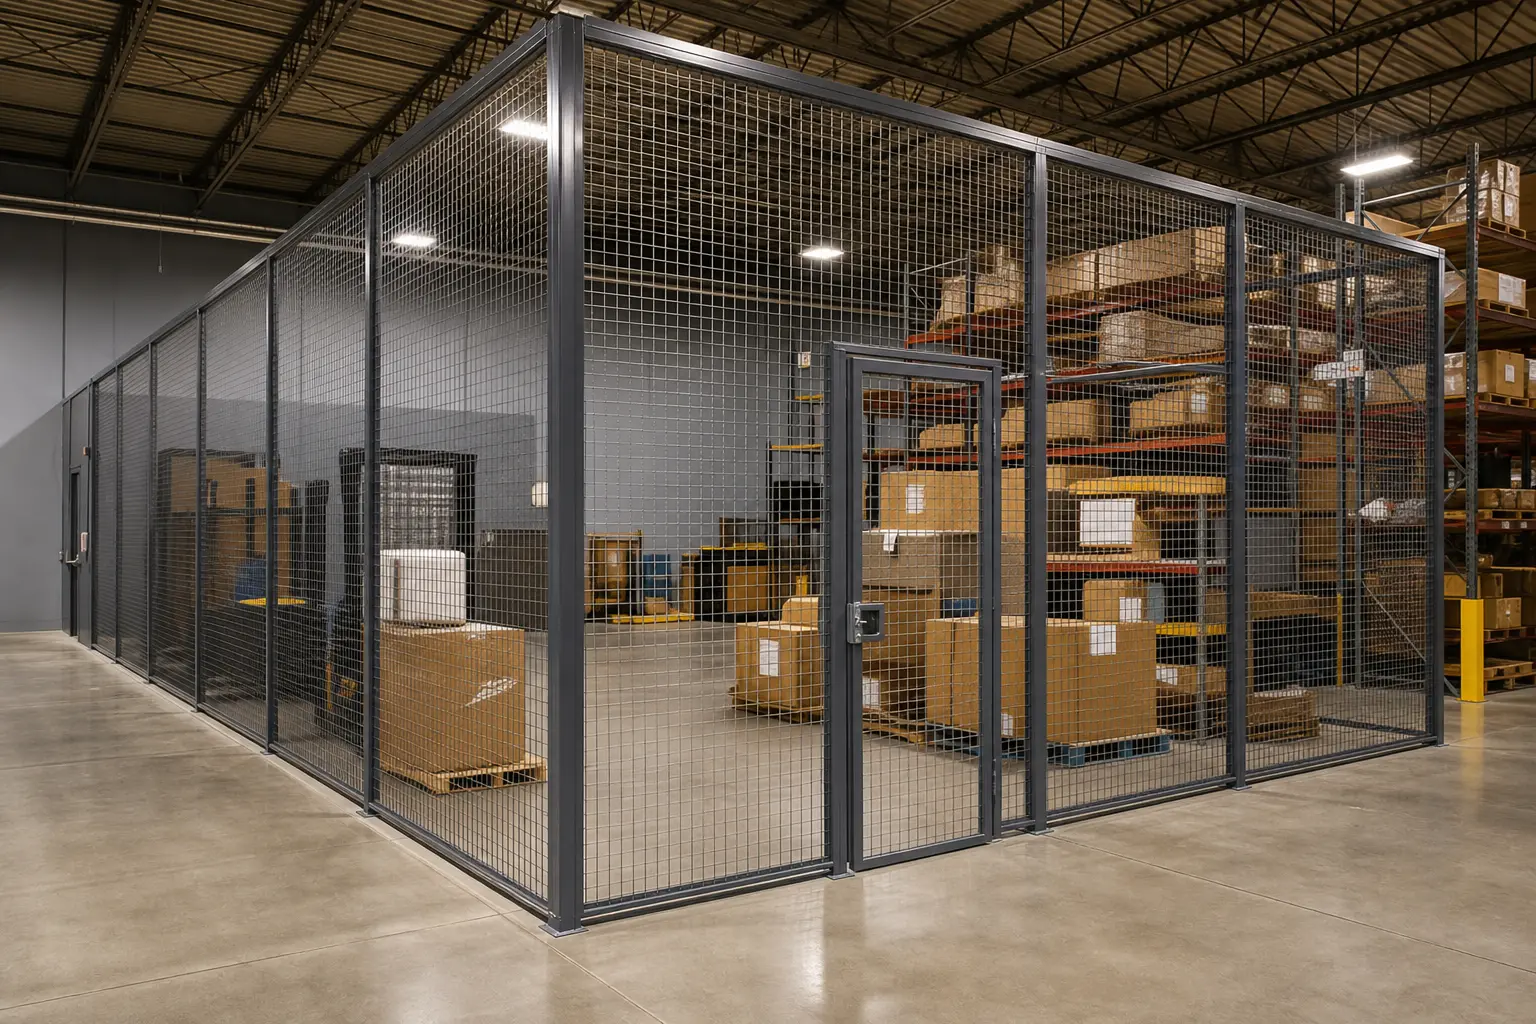
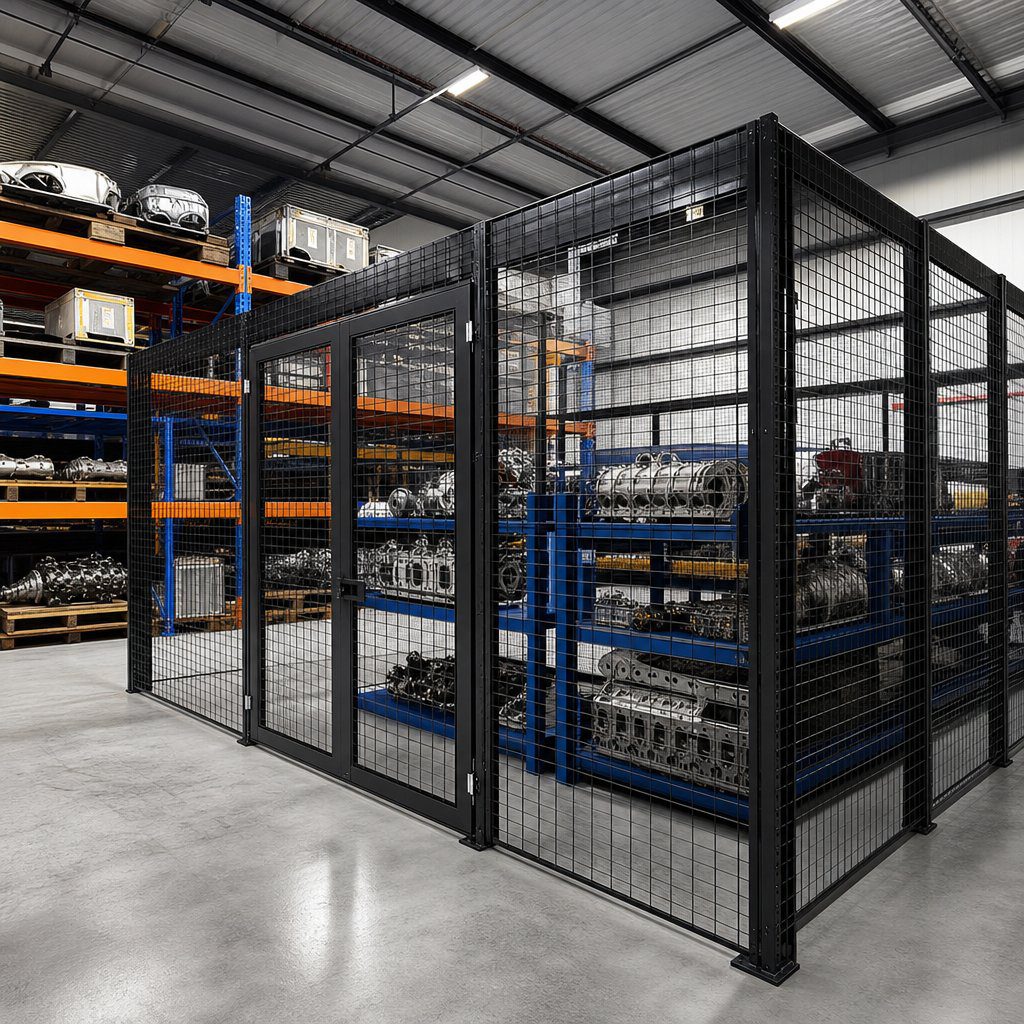
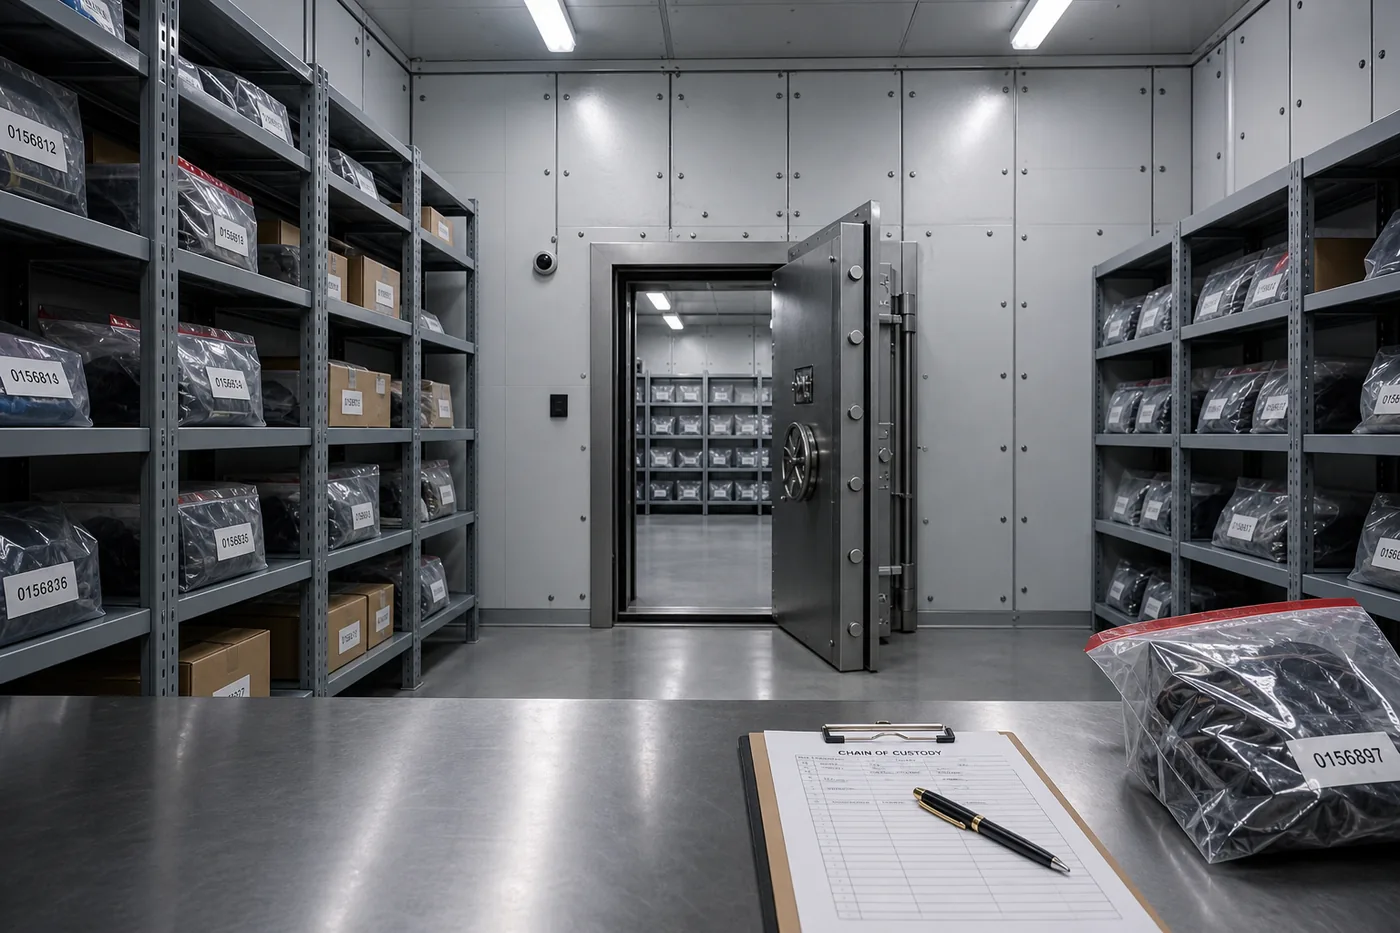

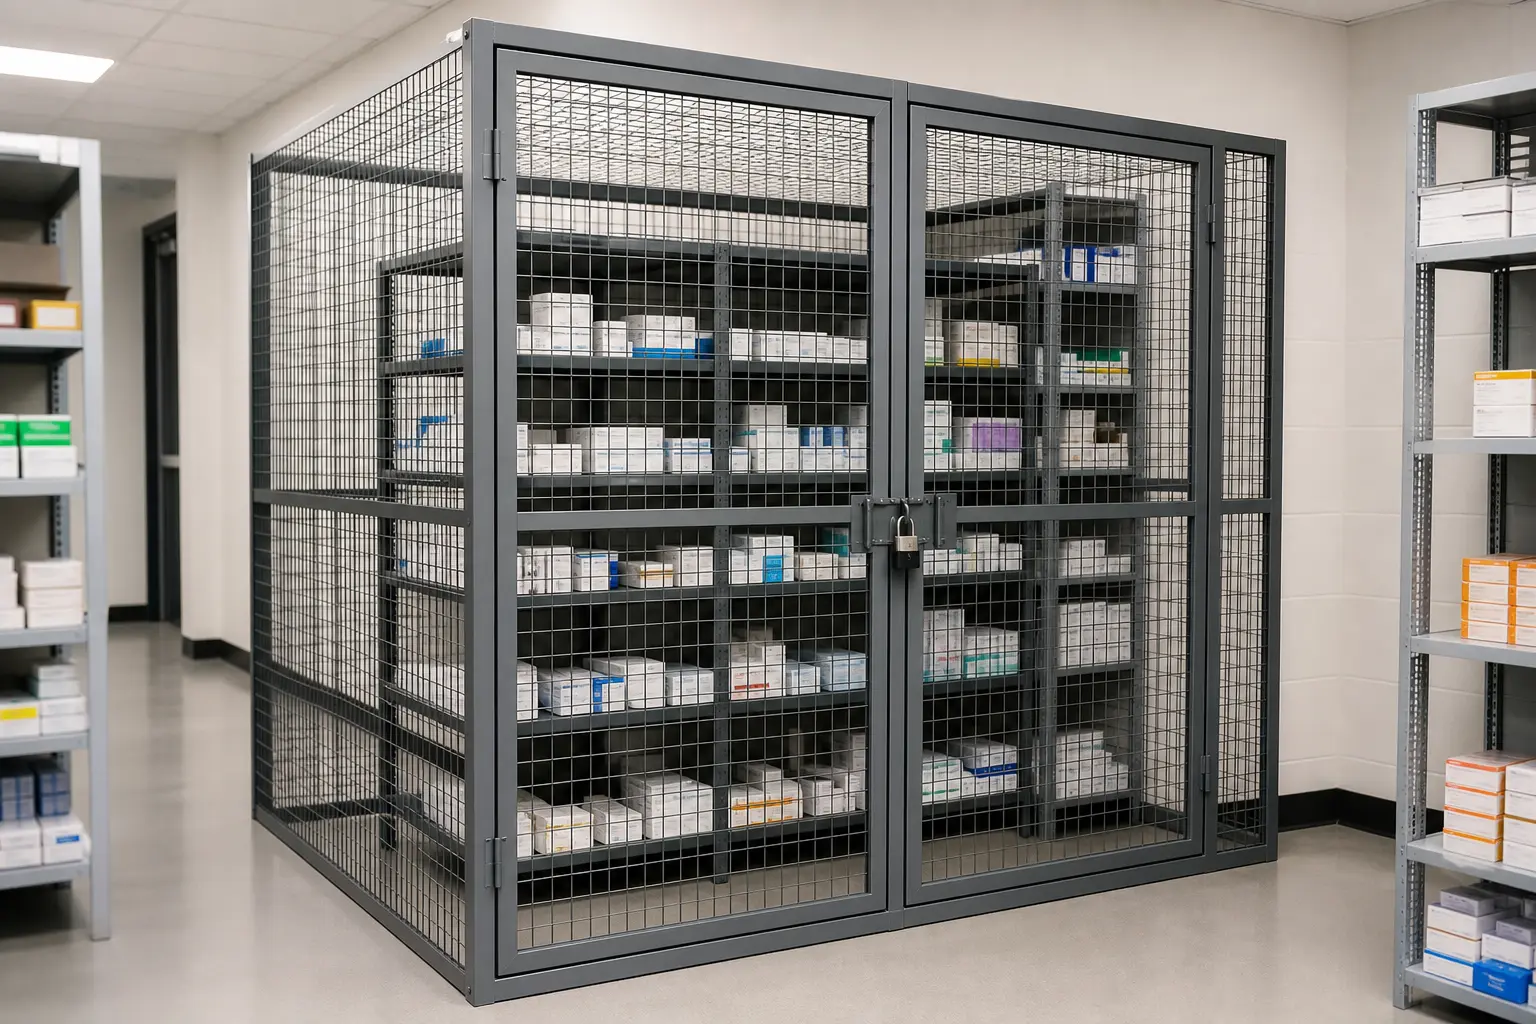
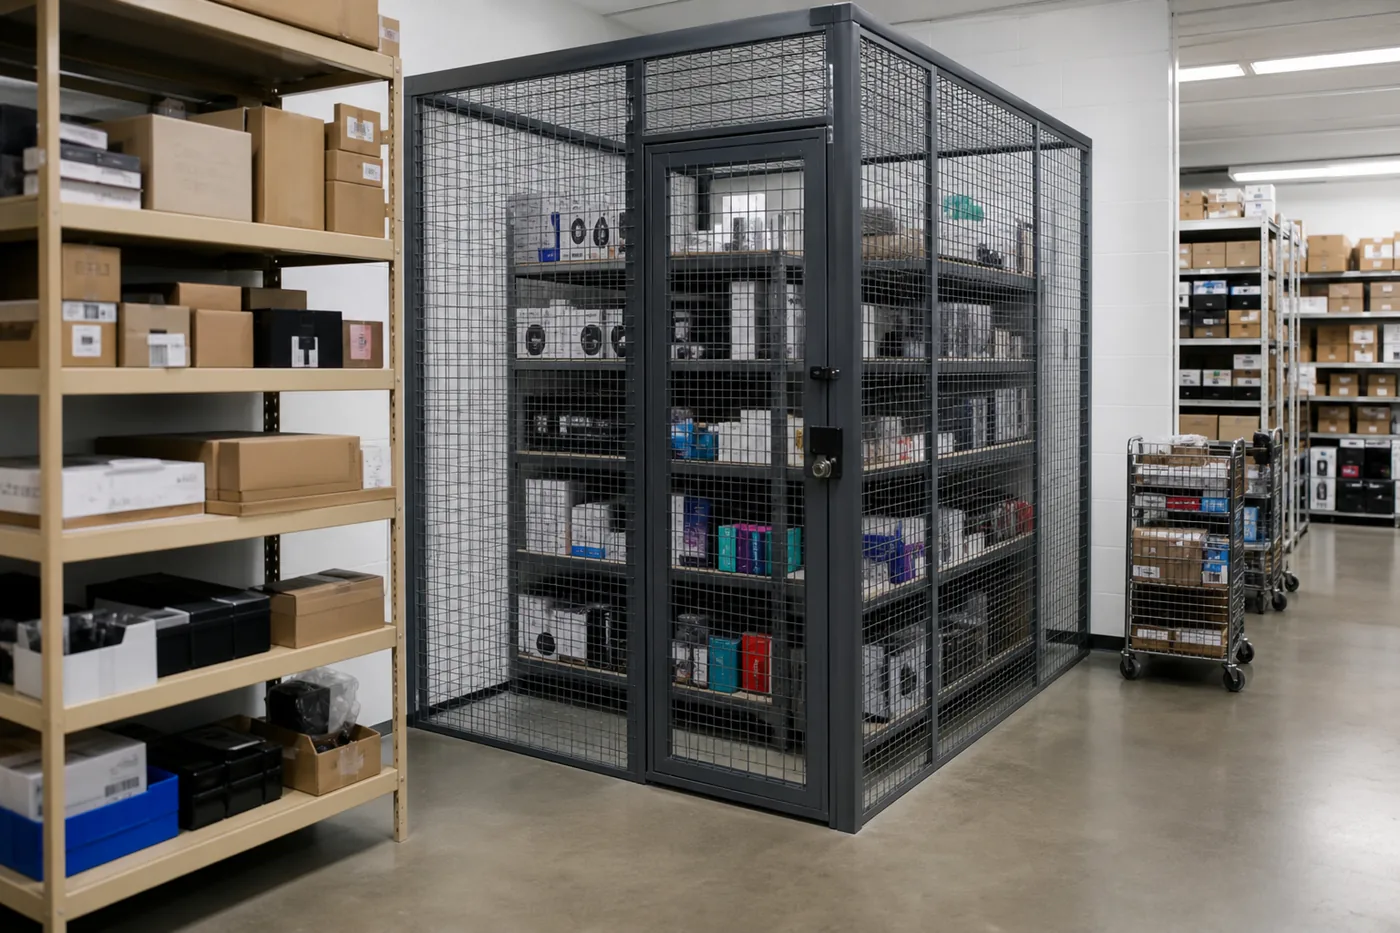


Any organization that needs to define boundaries, control access, and protect physical assets. That is the common thread. Wire enclosures are modular, so a cage can grow, shrink, or relocate as your operation changes — and because they preserve sightlines, sprinkler coverage, airflow, and lighting, they typically avoid the cost and permitting burden of a permanent wall.
The Strategic Advantages of Modular Wire Enclosures
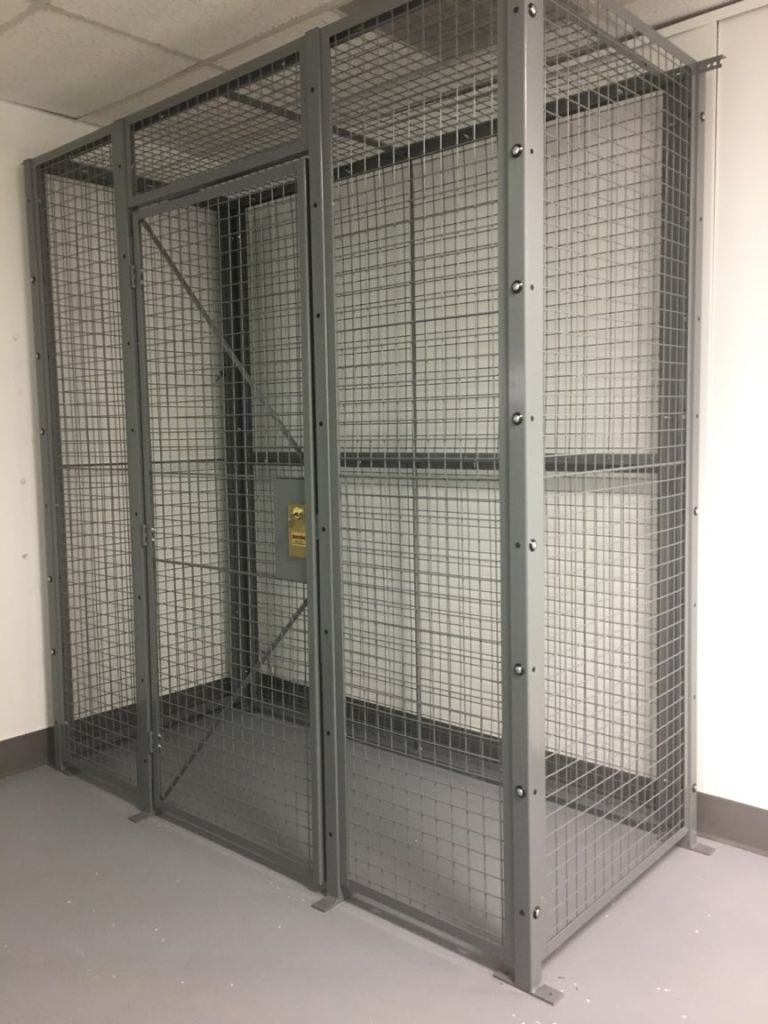
Choosing a security cage system from Material Handling USA offers numerous strategic advantages over traditional construction methods. The most immediate benefit is the significant cost savings. Building a permanent wall with studs and drywall is labor-intensive, messy, and permanent.
In contrast, our wire partitions are modular and can be installed in a fraction of the time—often just 1 to 2 days for standard configurations. This speed of installation minimizes disruption to your daily operations. Furthermore, because these systems are considered equipment rather than permanent building improvements, they often qualify for accelerated depreciation, providing a financial advantage at tax time.
Preserving HVAC, Lighting, and Sprinkler Infrastructure
Another major benefit is the preservation of facility infrastructure. Because our wire mesh allows for the free flow of air, light, and water, there is no need to relocate existing HVAC vents, lighting fixtures, or fire sprinkler heads. This “transparent” nature of the mesh also enhances safety by maintaining clear sightlines across the warehouse.
Supervisors can easily monitor activity inside the cage from a distance, which acts as a psychological deterrent to theft and ensures that safety protocols are being followed. The visibility also aids in inventory management, as staff can perform quick visual audits of stock levels without needing to unlock and enter the enclosure.
Durability and Powder-Coat Finishes
Durability and longevity are hallmarks of the brands we carry, such as BeastWire and SpaceGuard. Our steel partitions are finished with high-quality powder coatings that resist scratching, chipping, and corrosion, ensuring the system looks professional for years even in harsh industrial environments.
If your facility layout changes, the modular panels can be easily disassembled, moved, and reconfigured to fit a new space. This flexibility makes wire partitions a “future-proof” investment. Unlike a drywall room that must be demolished, a wire cage can grow and change alongside your business, providing a sustainable solution that reduces waste and long-term capital expenditure.
Turnkey Project Delivery
Finally, working with MH-USA means you benefit from our comprehensive, turnkey service. From the initial consultation and free layout design to the final professional installation, we handle every detail of the project. Our specialists are well-versed in local building codes and federal regulations, such as DEA requirements, ensuring that your installation is compliant from day one.
We provide a single point of contact for your security needs, integrating high-quality hardware, specialized gates, and even advanced locking mechanisms into a cohesive system. By choosing MH-USA, you are not just buying a product; you are gaining a partner dedicated to the security and efficiency of your industrial operations.
Benefits at a Glance
- Lower cost than permanent walls — no studs, drywall, or demolition when layouts change
- No infrastructure rework — mesh passes air, light, and sprinkler water, so HVAC and fire systems stay in place
- Built to last — powder-coated steel from BeastWire and SpaceGuard resists scratching and corrosion
- Turnkey delivery — free layout design through professional installation, handled by one team
Technical Specifications and Customization Options
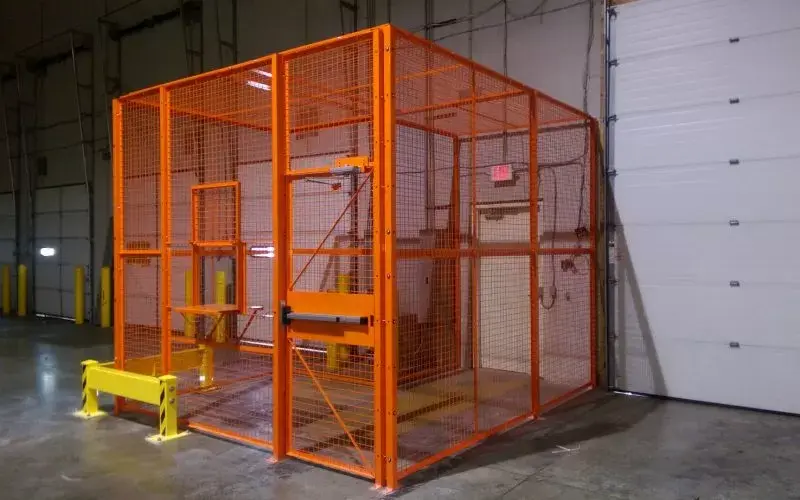
When designing a security enclosure, the technical specifications of the wire mesh and framing are the most critical factors in determining the system’s overall strength and effectiveness. At Material Handling USA, we offer a diverse range of specifications tailored to your specific security level. Our standard wire partitions typically utilize 10-gauge wire woven into a 2″ x 1″ rectangular mesh, though we also provide heavy-duty 6-gauge options for high-risk environments.
We partner with industry leaders like SpaceGuard and BeastWire to provide both woven and welded wire solutions. Woven wire offers a traditional, flexible strength ideal for general warehouse dividers, while welded wire provides a rigid, modern aesthetic that is increasingly popular for high-tech server rooms and data centers.
Framing, Posts, and Finish Options
Customization extends far beyond the mesh itself. The structural integrity of the cage is supported by cold-rolled steel posts and frames, which can be finished in a variety of ways to suit the environment. While a standard gray powder coat is the industry norm, we offer custom colors to match corporate branding or high-visibility safety yellow for industrial traffic areas.
For outdoor applications or wash-down environments, such as those found in chemical processing or coastal facilities, we provide hot-dipped galvanized finishes that resist corrosion and environmental wear. These frames are designed to be modular, allowing for easy expansion or reconfiguration as your facility’s needs evolve over time.
Doors, Gates, and Access Control
Access control is another area where customization is paramount. We offer a wide array of door configurations, including single and double swing doors, sliding doors with industrial-grade tracks, and even Dutch-style doors for service counters. To secure these entry points, we integrate everything from standard key locks and mortise cylinders to advanced electronic strikes and biometric scanners.
For facilities requiring maximum security, we can specify pick-resistant locks and heavy-duty shrouds that prevent tampering from the exterior. Our team works with you to determine the best hardware based on the frequency of use and the sensitivity of the items being stored.
Enclosure Sizing and Ceiling Heights
Finally, we address the physical dimensions and enclosure requirements of your space. While many applications only require a three-sided cage backed against an existing wall, we also design full four-sided enclosures and floor-to-ceiling partitions. If your facility has high ceilings, we can provide ceiling panels made of the same high-strength wire mesh to create a completely enclosed “six-sided” security room.
This prevents unauthorized access from above, which is a common requirement for high-value inventory and pharmaceutical storage. By utilizing brands like Jaken and Borroughs for internal shelving, we can even design the interior layout of the cage simultaneously with the exterior perimeter.
| Framing | Cold-rolled steel posts and frames with tamper-proof, inside-only hardware |
|---|---|
| Panel style | Open woven or welded wire mesh that passes air, light, and sprinkler water |
| Finishes | Standard gray powder coat, with custom colors available to match corporate branding |
| Door options | Single and double swing, sliding on industrial track, Dutch-style service doors |
| Access control | Padlock hasps through keyed cylinders and electronic strike locks |
| Enclosure types | Three-sided, full four-sided, and floor-to-ceiling partitions for high-bay spaces |
| Standards | DEA 21 CFR 1301.72, GSA / federal security protocols, OSHA machine guarding |
Professional Installation and Project Planning
The transition from a security concept to a fully realized physical enclosure requires meticulous project planning and professional execution. At Material Handling USA, our process begins with a comprehensive site evaluation and a free layout service. We utilize advanced CAD software to create detailed drawings that account for every obstacle in your facility, including HVAC ductwork, fire suppression sprinklers, electrical conduits, and lighting fixtures.
By identifying these potential conflicts during the design phase, we avoid costly delays and field modifications during the installation process. This proactive approach ensures that the final cage system fits perfectly within your existing footprint while maintaining all necessary clearances.
Delivery Coordination Around Your Operations
Once the design is finalized and the materials are sourced from top-tier manufacturers like Panel Built or SpaceGuard, our logistics team coordinates the delivery to coincide with your facility’s schedule. We understand that warehouse operations cannot simply stop for a construction project. Therefore, we offer flexible installation timelines, often completing standard configurations in just one to two days.
Our professional installation crews are highly experienced in handling heavy-duty wire panels and ensuring they are perfectly plumb and level. This precision is vital not only for the aesthetic of the cage but also for the smooth operation of sliding doors and the long-term durability of the locking mechanisms.
Anchoring and Seismic Stability
Anchoring and structural stability are the hallmarks of a professional installation. Our teams use heavy-duty wedge anchors to secure the vertical posts directly into the concrete floor, providing the lateral strength necessary to withstand impacts from forklifts or attempted breaches. In regions prone to seismic activity, we provide specialized footplates and bracing that meet local building codes and seismic requirements.
We also ensure that all hardware is installed with the “secure side” facing inward, utilizing carriage bolts and tamper-proof fasteners that cannot be removed from the outside of the enclosure. This attention to detail is what separates a professional security installation from a generic fencing job.
Final Walkthrough and Quality Assurance
The final stage of project planning involves a thorough walkthrough and quality assurance check. We test every door, lock, and sensor to ensure seamless operation and alignment. If your project involves modular buildings or integrated offices from Panel Built, we coordinate the interface between the wire partitions and the solid wall structures to ensure a seamless security perimeter.
Our goal is to provide a turnkey solution where the client only needs to provide the requirements, and we handle everything from the initial engineering to the final bolt. This comprehensive management style reduces the administrative burden on your facility managers and ensures a high-quality result every time.
Compliance, Safety, and Regulatory Standards
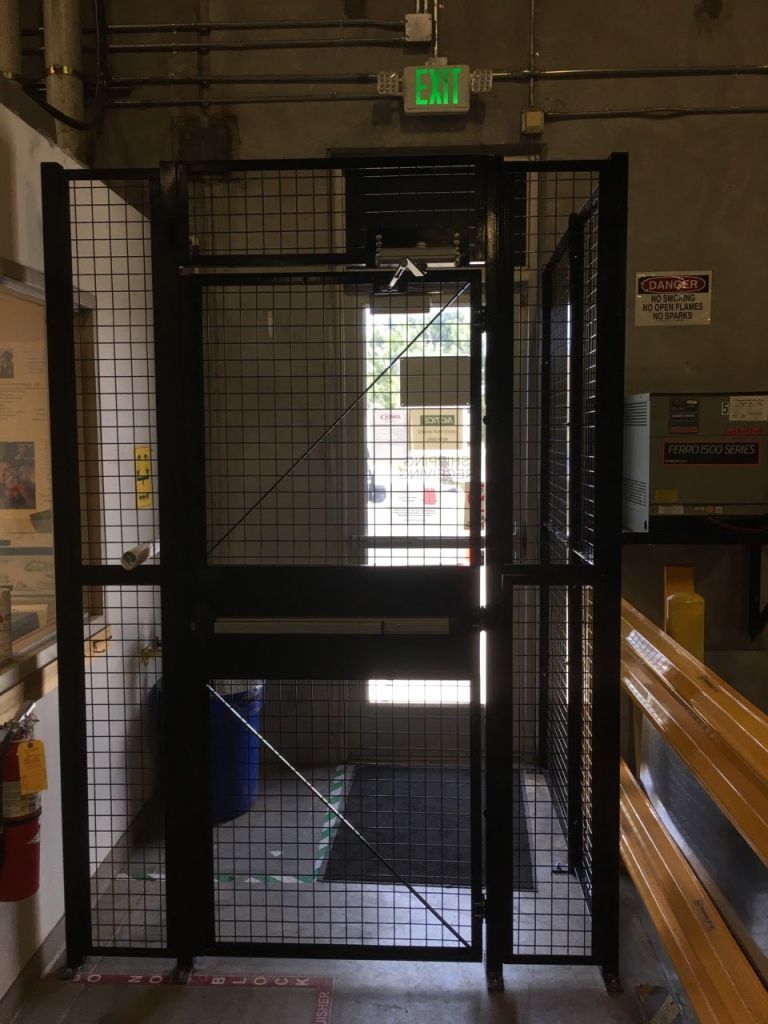
In many industries, a security cage is not just a theft deterrent; it is a legal or regulatory requirement. Material Handling USA specializes in designing enclosures that meet the stringent standards set by various governing bodies. For the pharmaceutical industry, we provide DEA-compliant cages that adhere to 21 CFR Part 1301.
These regulations require specific mesh sizes, typically no larger than 2 inches, and a maximum of 2 inches of “sweep” space between the floor and the bottom of the panels. Furthermore, these cages must include heavy-duty ceiling panels and self-closing, self-locking doors to ensure that controlled substances are protected at all times. Our expertise in these regulations ensures that your facility will pass inspection without the need for expensive retrofits.
Military and GSA Security Requirements
Beyond pharmaceutical requirements, we also cater to military and government sectors that demand high-security enclosures for sensitive equipment and classified documents. We utilize products from Dasco and BeastWire that are engineered to meet GSA standards and other federal security protocols.
These systems often feature reinforced frames and specialized locking hardware that can be integrated into a facility-wide security network. For evidence rooms in police departments, our cages provide a chain-of-custody environment that is both secure and transparent, allowing for visual inspections while preventing unauthorized handling of sensitive materials.
OSHA Machine Guarding
Safety standards also extend to the protection of personnel in industrial environments. OSHA (Occupational Safety and Health Administration) has strict guidelines regarding machine guarding and the separation of workers from hazardous equipment. Our wire partitions serve as effective physical barriers that prevent accidental contact with moving machinery or robotic cells.
By using brands like Metro and Aurora for integrated storage within these guarded areas, we help create a workflow that is both efficient and safe. The open-mesh design of our partitions also ensures that fire suppression systems remain effective, as water from overhead sprinklers can easily pass through the wire to reach the source of a fire, unlike solid-walled rooms.
Egress and Local Fire Code
Finally, we consider the structural safety and fire codes of the local municipality. Our designs account for “egress” requirements, ensuring that personnel inside a large enclosure can exit quickly in the event of an emergency. This often involves the installation of panic bars or “push-to-exit” hardware on the interior of the cage doors.
We also ensure that the height of the partitions does not interfere with existing smoke detectors or ventilation systems. By balancing the need for high security with the necessity of life safety and fire code compliance, Material Handling USA provides a holistic solution that protects your assets, your employees, and your legal standing.
Compliance Checklist for Your Enclosure
- DEA 21 CFR 1301.72 construction requirements for controlled-substance storage
- GSA and federal security protocols for government and military installations
- OSHA machine guarding and worker separation from hazardous equipment
- Egress planning with panic bars or push-to-exit hardware on large enclosures
- Local fire code review, including sprinkler and lighting pass-through
- Wedge anchoring and seismic bracing appropriate to your region
Why Choose Material Handling USA for Your Security Needs
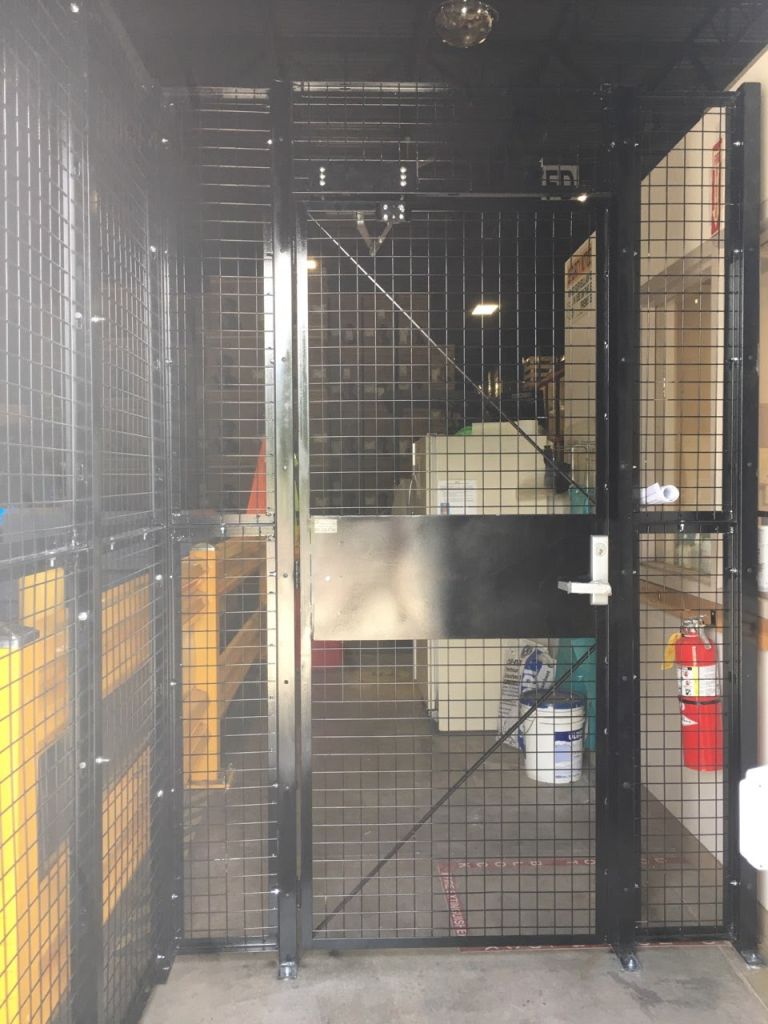
Choosing a partner for your facility’s security is a decision that impacts your operational efficiency and asset protection for years to come. Material Handling USA stands out in the B2B marketplace because we combine decades of industry expertise with a massive catalog of high-quality products. We are not just a reseller; we are a full-service solutions provider.
By maintaining strong relationships with premier manufacturers like SpaceGuard, BeastWire, Panel Built, and Borroughs, we are able to offer competitive pricing and shorter lead times than many of our competitors. Our deep understanding of the material handling industry allows us to see the “big picture,” ensuring that your security cage integrates perfectly with your shelving, pallet racking, and modular office systems.
A Consultative, Specialist-Led Process
Our consultative approach is what truly sets us apart. When you call (800) 326-4403, you aren’t just talking to a salesperson; you are talking to a specialist who understands the nuances of warehouse logistics and industrial security. We take the time to understand what you are securing—whether it’s high-value electronics, hazardous chemicals, or sensitive data—and we recommend the specific gauge, mesh, and locking system that fits that need.
We avoid the “one size fits all” mentality, instead focusing on a custom-engineered solution that maximizes your ROI. This level of personalized service is why companies across the United States trust us with their most critical security projects.
Turnkey From Layout to Installation
Furthermore, our commitment to a “turnkey” experience means we handle the complexities so you don’t have to. From the initial free layout and CAD design to the final professional installation, we manage every detail of the project. This includes navigating the complexities of DEA compliance or OSHA safety standards, which can be a daunting task for facility managers.
We also offer a wide range of complementary products, such as Metro wire shelving or Aurora mobile filing systems, which can be installed inside your new cage to create a fully organized and secure storage environment. This ability to source and install everything from a single point of contact simplifies your procurement process and ensures a cohesive final result.
Reliability and Industrial-Grade Materials
Ultimately, Material Handling USA is built on a foundation of reliability and professional integrity. We understand that in the B2B world, downtime is expensive and security breaches are unacceptable. That is why we only use industrial-grade materials and proven installation techniques. Our goal is to build long-term partnerships with our clients, providing them with the equipment and expertise they need to grow their businesses safely and efficiently.
Whether you are a small local distributor or a large-scale manufacturing plant, we provide the same level of dedication and technical excellence to every project. Contact us today at Sales@MH-USA.com to experience the difference that professional material handling expertise can make for your facility.
Frequently Asked Questions
Are your security cages DEA compliant for pharmaceutical storage?
Can wire partitions be customized for irregular room layouts?
Do you provide professional installation services?
What is the difference between woven and welded wire mesh?
How long does it take to receive a custom security cage quote?
Secure Your Facility with a Custom Quote Today
Ready to protect your inventory, sensitive data, or controlled substances? Contact our material handling specialists at (800) 326-4403 or email Sales@MH-USA.com to receive your free layout and a comprehensive quote on a custom wire partition system.