
In-Plant & Industrial Modular Buildings
Factory-built panel buildings assembled inside your plant or warehouse, or outside on your site: control rooms, cleanrooms, equipment enclosures, break rooms and in-plant offices. Installed in days, relocatable when your layout changes.
Talk with a specialist. Call (800) 326-4403 or email Sales@MH-USA.com

Looking for an office inside your warehouse or plant?
Our modular in-plant offices page covers single and two-story offices, wall panels, windows, doors and storage roofs. This page covers the full range of in-plant and industrial modular buildings, from control rooms to equipment enclosures. For shipping offices, supervisor stations and two-story offices on the warehouse floor, see our guide to modular offices for warehouses.
Prefabricated Modular Building Solutions

Modular buildings deliver permanent-quality construction with less disruption and a shorter on-site schedule than conventional construction, priced per configuration. Material Handling USA partners with a leading U.S. modular building manufacturer to deliver custom modular structures for warehouses, manufacturing plants, distribution centers, and industrial facilities nationwide.
Every modular building uses a proprietary wall panel system — steel-skinned, foam-core insulated panels that interlock into a rigid, climate-controlled enclosure. Structures ship as flat-pack panels and assemble on-site in days with basic tools and a small crew. No concrete block, no drywall mud, no weeks of finish carpentry.
Applications range from simple 10×12 foreman offices to complex multi-room cleanroom suites with ISO-rated HVAC, fire suppression, and environmental monitoring. Whatever your facility needs, modular construction gets you there faster and at lower cost.
Modular Building Types
We supply every type of modular structure for industrial and commercial facilities.


Why Material Handling USA for Modular Buildings
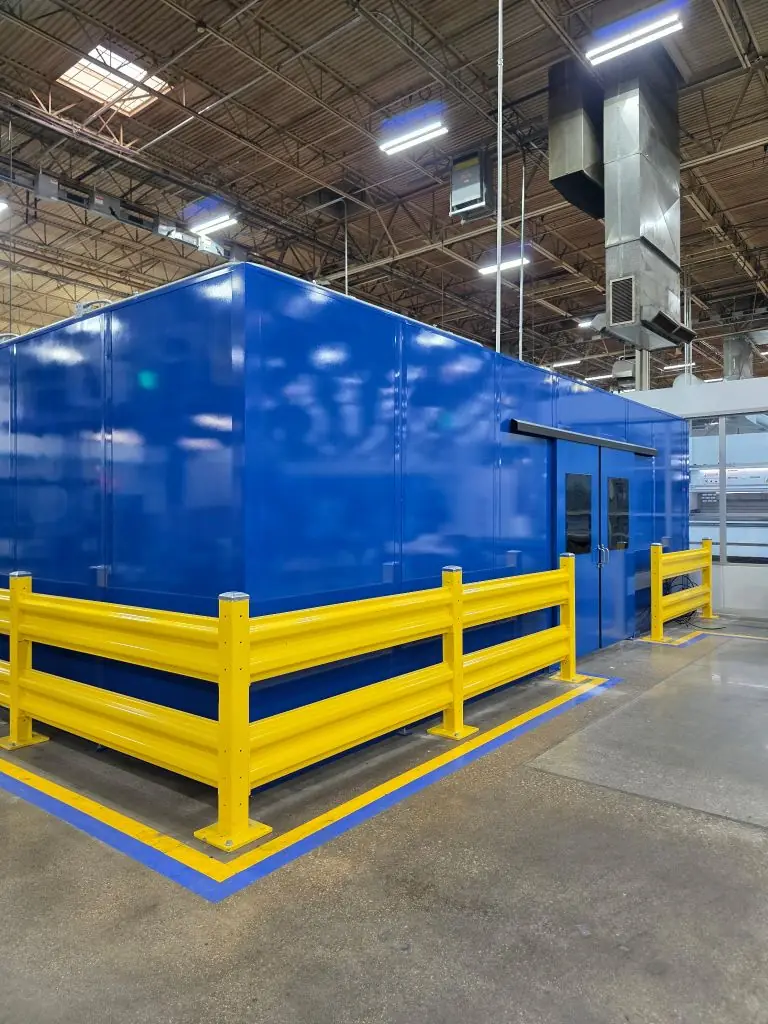
Our manufacturing partner has built modular buildings since 1995 in their Blairsville, Georgia production facility. Their proprietary wall panel system uses 2″ or 3″ thick foam-core panels bonded between steel or FRP skins, creating rigid, insulated wall sections that interlock with cam-lock fasteners for rapid assembly. More on the manufacturer is on our Panel Built page.
Standard features include commercial-grade electrical systems (100–400 amp), HVAC systems sized for the building volume, LED lighting, and fire alarm/sprinkler rough-ins. Panels come pre-wired and pre-finished — no painting, no drywall, no electrical rough-in on site.
Our manufacturer partner’s engineering team produces stamped structural drawings, electrical layouts, mechanical plans, and code compliance packages for every project. Their modular approach means structures can be expanded, reconfigured, or relocated as your facility needs change.
Standard & Available Features
Every modular building is custom-configured with these available options.

- Wall Panel Systems — 2″ and 3″ foam-core panels with steel, FRP, vinyl, or stainless skins. R-16 to R-40 insulation values. Class A fire-rated options available.
- HVAC & Climate Control — roof-mounted or remote HVAC units sized for building volume. Cleanroom HEPA/ULPA filtration, temperature/humidity control for critical environments.
- Electrical Systems — pre-wired 100–400 amp panels, LED lighting, emergency lighting, GFCI outlets, and conduit runs for data, phone, and security systems.
- Fire Protection — UL-classified 1, 2, and 4-hour fire-rated assemblies. Sprinkler rough-ins, fire alarm panels, and emergency exit lighting included.
- Sound Attenuation — STC rating depends on panel construction; ask for the rated assembly. Acoustic wall panels, sealed penetrations, and vibration isolation for equipment enclosures.
- Windows & Doors — commercial aluminum-frame windows, hollow-metal doors, sliding doors, and roll-up doors. Ballistic-rated and blast-resistant options available.
Why Modular Over Conventional Construction?
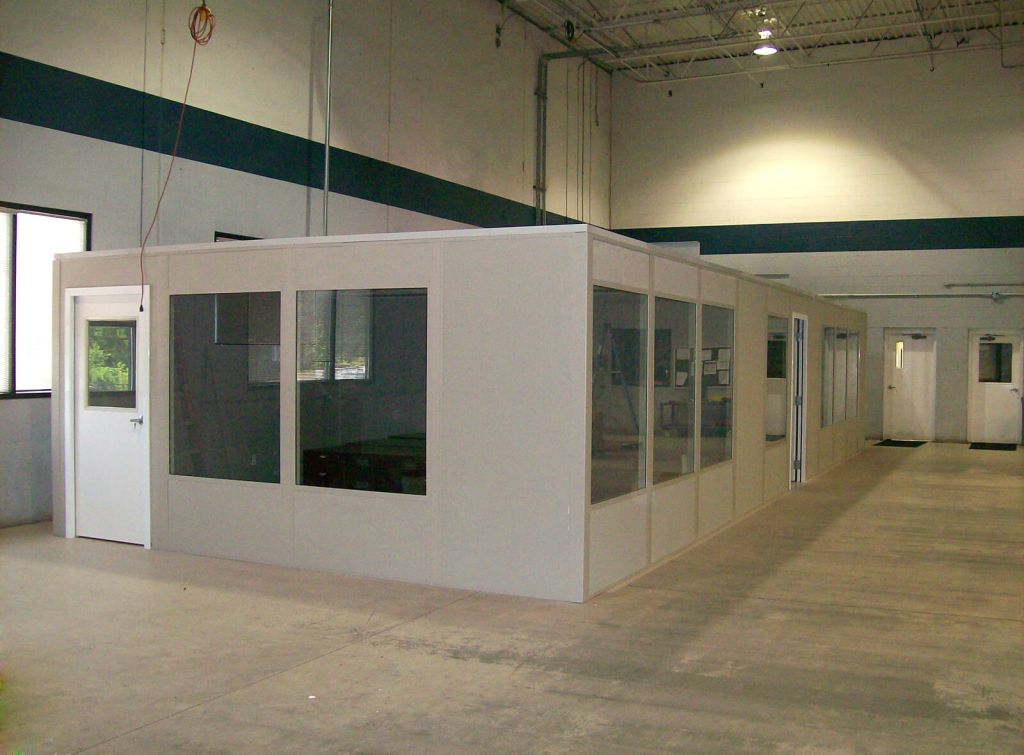
Modular buildings are usually ready for use much sooner than conventional construction. While your site pad is being prepared, your building is fabricated in a climate-controlled factory — weather delays don’t exist. Installation typically takes 3–10 days depending on building size and complexity.
Total project cost is often lower than stick-built construction once downtime and trade coordination are counted. Factory fabrication eliminates waste, rework, and the coordination complexity of multiple subcontractors. You get a fixed price, a guaranteed timeline, and a building that meets the same codes as conventional construction.
Modular buildings are also classified as equipment, not real property, which can provide significant tax advantages through accelerated depreciation. They’re relocatable capital assets that move with your business rather than fixed improvements attached to someone else’s landlord.
From Concept to Completion
Your modular building project in four straightforward steps.
Needs Assessment
We evaluate your space requirements, environmental conditions, code requirements, and utility connections to recommend the optimal configuration.
Engineering & Design
Detailed construction drawings, structural calculations, electrical/mechanical plans, and permit-ready documentation from licensed engineers.
Factory Fabrication
Panels manufactured, pre-wired, pre-finished, and quality-inspected in a climate-controlled factory. No weather delays or field rework.
Site Delivery & Assembly
Flat-pack panels ship by truck and assemble on your prepared slab. Most buildings complete in 3–10 days with a small crew.
Design Your Modular Building Online
Configure your modular in-plant office, guard booth, or cleanroom with our free interactive configurator. Choose dimensions, wall systems, doors, HVAC, and electrical — see a live preview and get an instant bill of materials.
Free online tool — no account required | View All Design Tools
Protect In-Plant Buildings: Bollards, Handrail and Corner Guards
In-plant modular buildings are quoted per project and are not sold online. These steel bollards, handrail and corner guards help protect a new building's corners, walls and door from forklift traffic, and they can be ordered online.
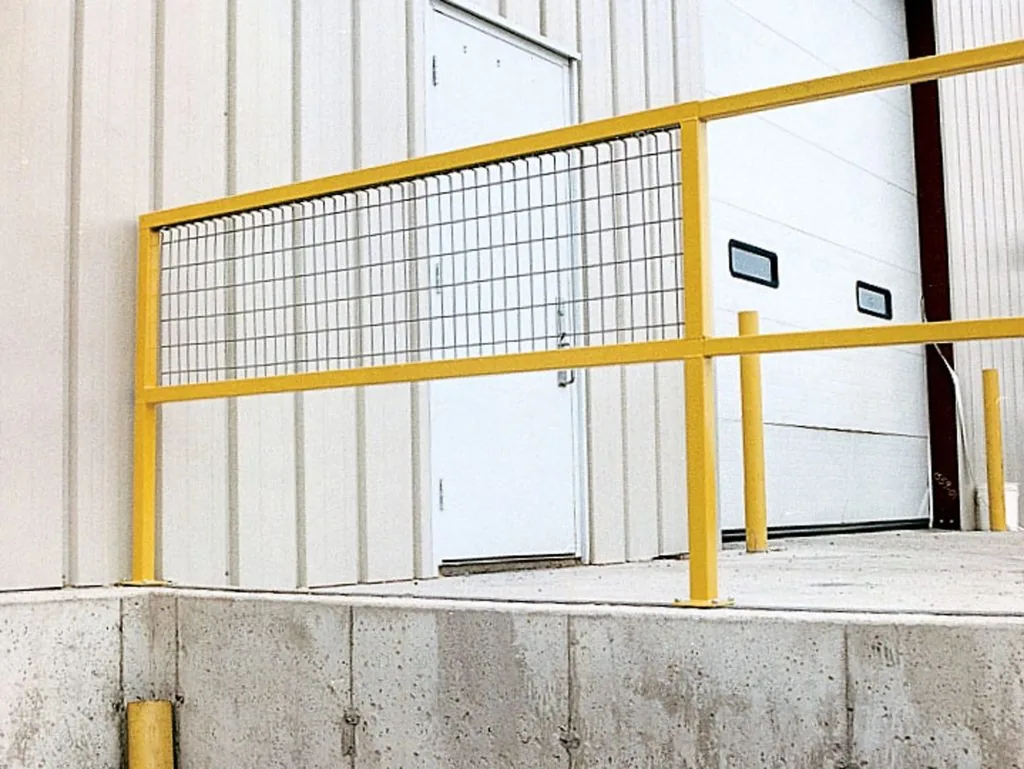

Browse all protective barriers, or read our guide to forklift protection for in-plant offices.
Modular Building Applications
Guides for the building types, industries and planning questions we see most often. Start with the room you need, then check the specification topics that apply to your site.
Building Types & Room Applications
- Prefabricated control buildingsSiting, blast and pressurization for process control rooms
- Modular electrical houses (e-houses)Walk-in buildings laid out around switchgear
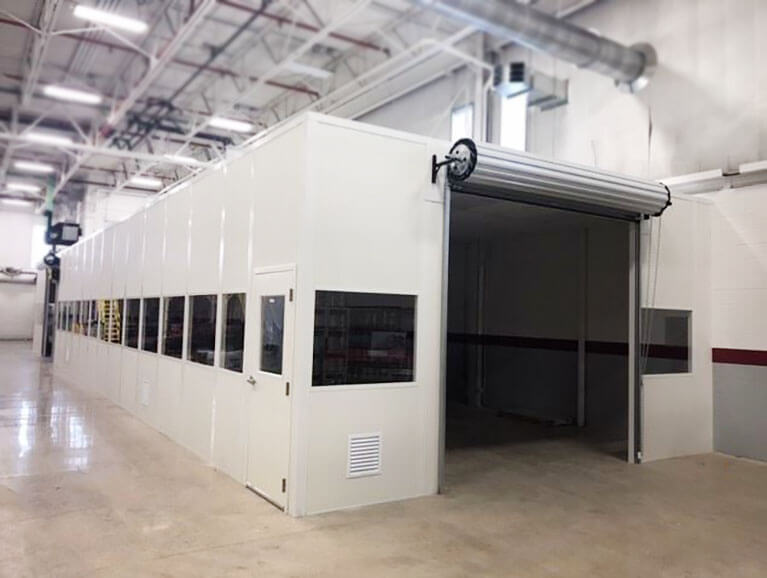
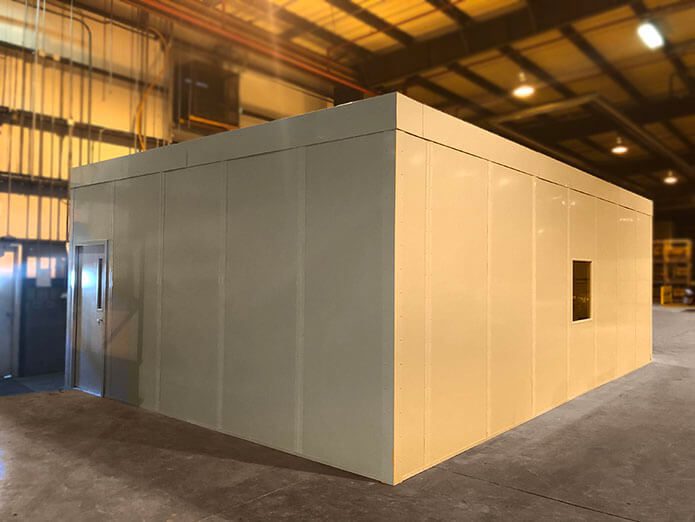
- Equipment enclosures and machine roomsPanel-built rooms around machinery, indoors or out
- Sound enclosures and acoustic roomsContaining machine noise or creating quiet rooms
- Modular cleanroomsHardwall ISO-classified rooms for manufacturing and pharma
- Modular restroomsIndoor prefabricated restrooms for plants and warehouses
- Break rooms and conference roomsSound-rated lunch and meeting rooms on the plant floor
- Two-story modular officesTwo levels of offices or meeting space in one footprint
- Modular office with storage roofLoad-bearing roof deck for storage above the office
- Lactation rooms and nursing podsPrivate, locking rooms for warehouses, plants and offices
- Fire-rated in-plant officesWhen an office needs rated walls, doors and glazing
- Ballistic-rated buildingsBullet-resistant booths, gate houses and enclosures
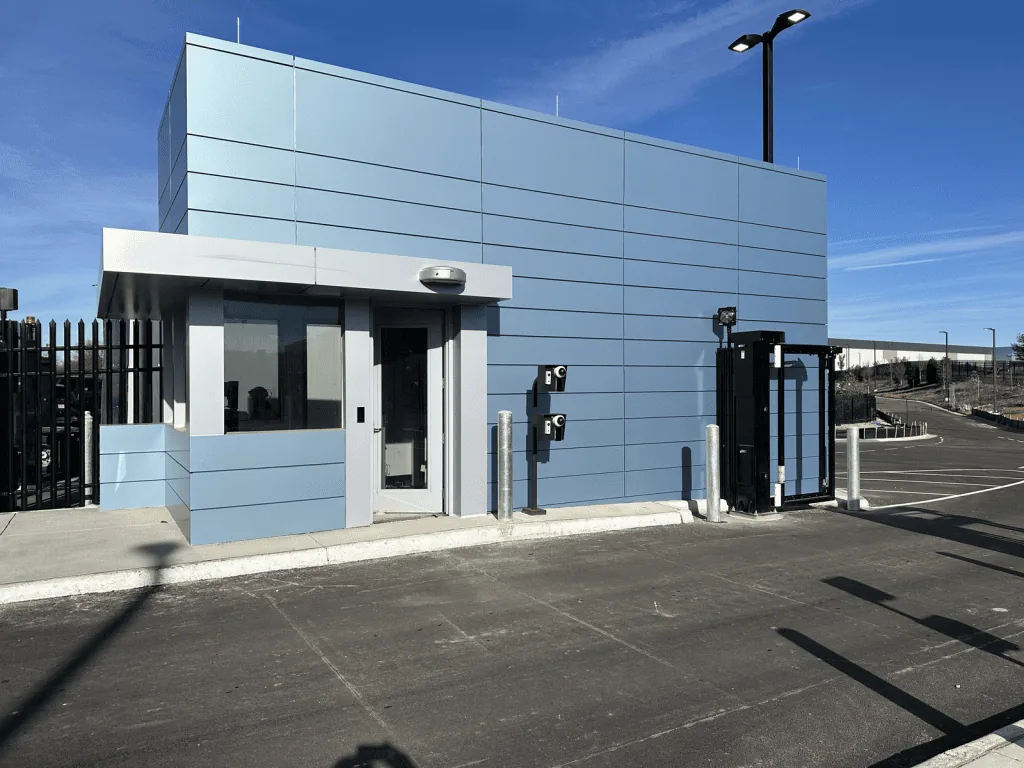
- Prefab guard booths and security shacksGate, truck-entrance and yard checkpoint buildings
- Guard and observation towersEnclosed cabs on engineered steel towers
- Prefabricated exterior buildingsOutdoor offices, operator and equipment buildings
- School press boxesSightlines, working space and services for stadium press boxes
- Modular vaults and secure roomsRated secure rooms without poured concrete
- Relocatable modular buildingsStructures designed to be moved when layouts change
- Commercial modular buildingsOffices and facility expansion beyond the plant floor
- Energy-efficient modular buildingsInsulation, HVAC and lighting choices that cut operating cost
Modular Buildings by Industry
- Manufacturing plantsIn-plant offices, QC rooms and clean assembly rooms
- Food and beverage plantsCleanable production offices, QA labs and packaging rooms
- Pharmaceutical and life sciencesCleanrooms, QC labs, gowning and controlled storage
- Healthcare and hospitalsAdmin offices, medical storage and screening buildings
- Data centersSecurity booths, NOC rooms and secure storage
- Distribution centers and 3PLsShipping offices, driver check-in and dispatch rooms
- Cold storage and freezer facilitiesVapor barriers, dew point and freezer slab details
- Combustible-dust facilitiesOffices and control rooms in classified dust areas
- Aviation and airportsHangar offices, operations rooms and gate buildings
- Water and wastewater plantsPump station, electrical and control buildings
- Oil, gas and energyControl rooms, e-houses and skid-mounted enclosures
- Construction and mining sitesField offices, change houses and electrical buildings
- Government and militaryEntry control booths, towers and support buildings
- Schools and universitiesPress boxes, ticket and security booths, storage
- Cannabis and controlled-environment agricultureGrow, drying, processing and secure storage rooms
Planning, Specifying & Buying
- Modular building buyer’s guideFrom requirements and quotes to design approval
- Modular building cost guideSize, layout, HVAC, ratings, freight and site work
- Lead times, delivery and installationHow long design, fabrication and install take
- How modular buildings are installedSite prep to final walk-through, step by step
- How modular buildings are manufacturedPanel fabrication, factory wiring and QA
- Permits and code compliancePlan review, codes and third-party inspection
- Specifying for architects and design teamsMasterFormat sections, delegated design and submittals
- Modular building specificationsLayout, assemblies and services for industrial rooms
- Interior specificationsWalls, ceilings, electrical, HVAC and finishes
- Press box specificationsLayout and features for stadium press boxes
- Seismic design and anchorageHow offices are anchored and braced in seismic zones
- Foundation and anchoring optionsExisting slab, piers, gravel pads and new slabs
- Financing, leasing and tax questionsWays to pay and what to ask your advisor
Components, Options & Comparisons
- Wall panels and insulationPanel construction, R-values and sound ratings
- Doors and windowsDoor types, hardware, access control and glazing
- Roofing and weather protectionLay-in ceilings, storage roofs and exterior roofs
- Flooring optionsSealed concrete, VCT, vinyl, carpet tile and raised floors
- Electrical systems and wiringLoad centers, lighting, data and three-phase power
- HVAC optionsWall units, mini-splits, ducted and rooftop systems
- Fire suppressionSprinklers and clean-agent systems inside modular rooms
- Ballistic ratings guideUL 752 levels explained for booths and buildings
- Custom finishes and brandingPanel skins, brand colors, ceilings and floors
- Modular office vs drywall buildoutSchedule, disruption, cost and permits compared
- Modular buildings vs shipping containersSize, insulation and use inside plants
- Modular buildings vs portable office trailersRental vs ownership, comfort and placement
- Complete modular building indexEvery modular building page in one place
Modular Building Case Studies
Real projects from mine sites, plants, garages and marine installations.
Modular Building FAQs
How long does a modular building take?
Typical lead time is 4–8 weeks from order to installation. Some simple structures can ship sooner, subject to confirmation. Complex cleanroom or fire-rated buildings may take 8–10 weeks.
Are modular buildings up to code?
Yes. Every structure is engineered to IBC code and stamped by a licensed structural engineer. We provide complete permit packages including structural, electrical, and mechanical drawings.
Can modular buildings be expanded later?
Yes. The panel system is designed for future expansion. Additional wall sections, rooms, and floors can be added without disrupting existing operations.
What sizes are available?
Standard panels allow buildings from 8×8 single-room offices to 100×200+ multi-room facilities. There is no practical maximum size — larger structures use multiple shipping loads.
How do modular buildings compare to trailers?
Modular buildings are permanent-quality structures with 20+ year lifespans, proper insulation, commercial HVAC, and code-compliant construction. Trailers are temporary structures with 5–10 year useful lives and limited customization.
Cleanroom & Controlled Environment Design
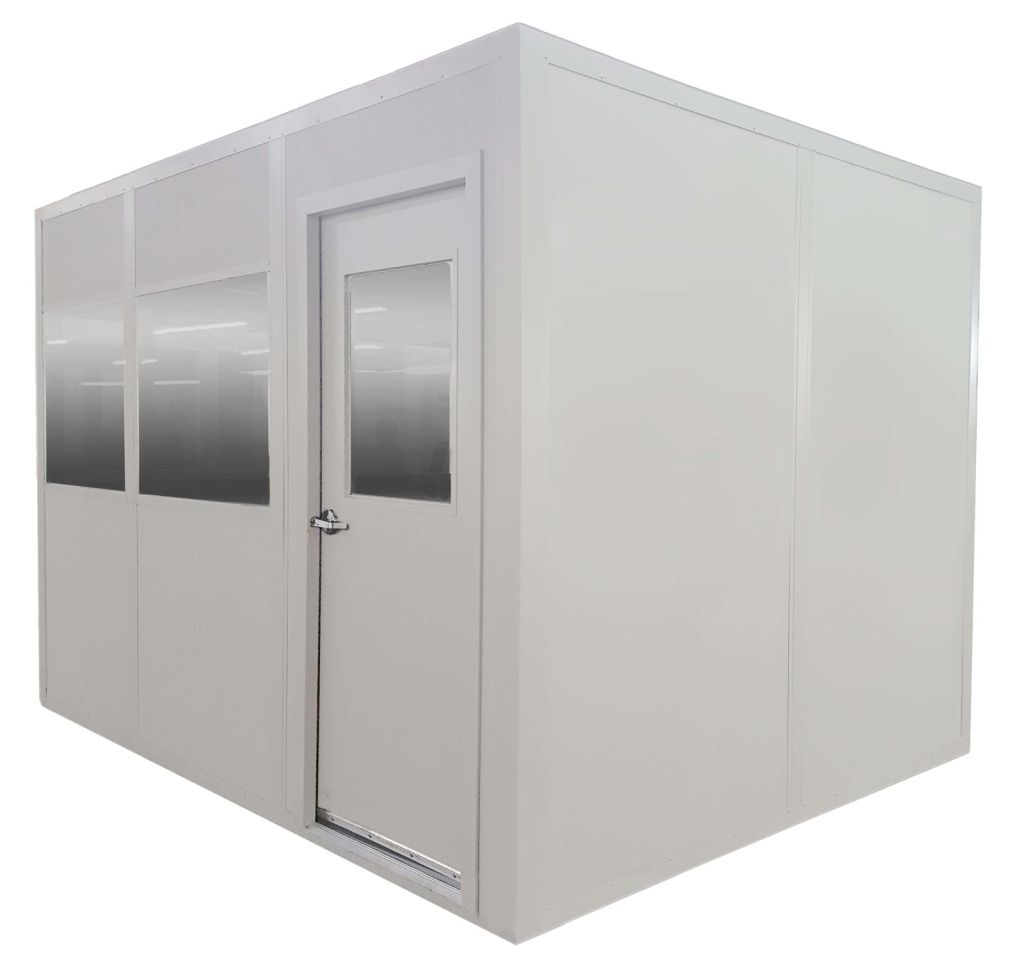
Our modular cleanrooms are built for ISO Class 5 through Class 8 air cleanliness requirements, usually with a shorter on-site schedule and less disruption than conventional cleanroom construction. The modular wall panel system creates rigid, sealed enclosures with flush interior surfaces that resist particle accumulation and simplify cleaning protocols. HEPA and ULPA filtration systems are ceiling-mounted in fan-filter units (FFUs) that provide laminar or turbulent airflow depending on the ISO classification required.
Cleanroom HVAC design addresses four critical parameters: particulate filtration (HEPA 99.97% at 0.3 microns for ISO 7, ULPA 99.999% for ISO 5), temperature control (typically 68°F ±2°F), humidity control (typically 30–60% RH), and pressure differential (positive pressure versus adjacent spaces to prevent unfiltered air infiltration). The mechanical engineers calculate air change rates, filter sizing, and system redundancy for each cleanroom based on its ISO classification and operational requirements.
Modular cleanrooms are particularly advantageous for pharmaceutical, medical device, and electronics manufacturing because they can be validated and qualified more quickly than conventional construction. Since the wall system is standardized and pre-tested, IQ/OQ/PQ protocols are streamlined. Modular cleanrooms can also be disassembled and relocated if production moves to a new facility — preserving a capital investment that conventional construction would forfeit.
Gowning rooms, air showers, pass-throughs, and material air locks are designed as integral components of the cleanroom system. The team engineers the entire cleanroom suite — from the dirtiest corridor space through progressive gowning stages to the cleanest production area — ensuring proper pressure cascades and personnel/material flow patterns that prevent cross-contamination.
In-Plant Office Design & Configuration

In-plant modular offices are the most common modular building application — creating climate-controlled office space inside warehouses, factories, and distribution centers without sacrificing production floor area. Standard configurations range from single-room supervisor stations (8×10) to multi-room office suites (40×60+) with conference rooms, break rooms, restrooms, and server closets.
The modular wall panel system provides good sound attenuation; the STC rating depends on panel construction, so ask for the rated assembly when you have a noise target. This means conversations inside the office remain private despite the noise of forklifts, conveyors, and production equipment on the other side of the wall. For applications requiring higher sound isolation (call centers inside manufacturing plants, for example), acoustic panel upgrades with additional mass and damping layers are available.
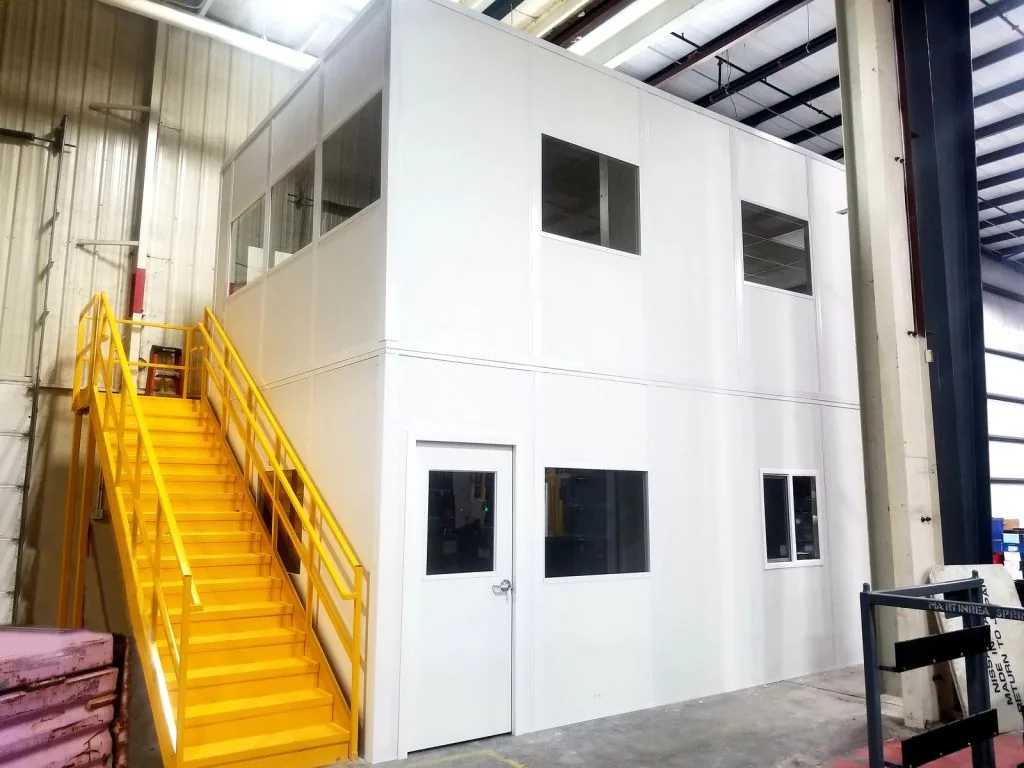
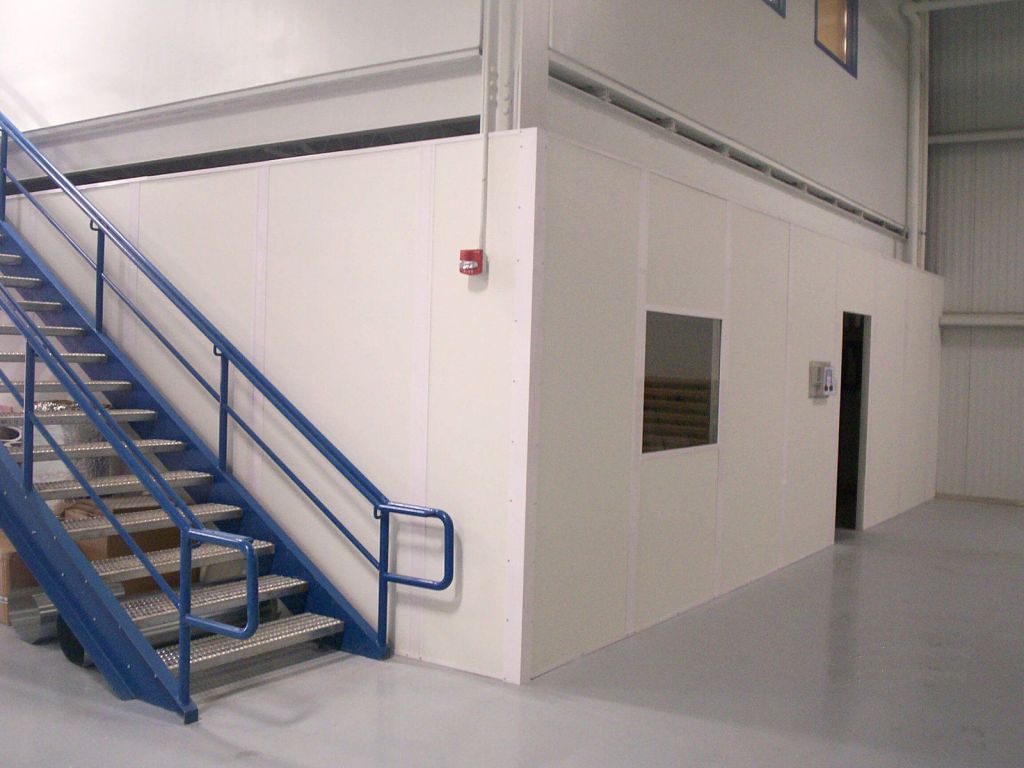
Multi-level modular offices are built on structural steel mezzanines to create two-story office buildings inside warehouse spaces. The ground floor houses the mezzanine-supported office, while the mezzanine level above provides additional office space, storage, or observation platforms overlooking the warehouse floor. This configuration maximizes the use of vertical space while keeping management offices physically connected to operations.
Modular Building Specifications
Compare key specifications across common modular building applications.
| Feature | Standard Office | Cleanroom | Fire-Rated | Equipment Enclosure |
|---|---|---|---|---|
| Wall Panels | 2″ foam core | 2–3″ flush | UL rated | 2–3″ steel skin |
| Insulation | R-16 | R-16 to R-32 | R-16+ | R-16 to R-40 |
| HVAC | Roof unit | HEPA FFU | Standard | Exhaust + cooling |
| STC Rating (ask for the rated assembly) | Depends on panel build-up | Depends on panel build-up | Depends on panel build-up | Depends on panel build-up |
| Fire Rating | N/A | Optional | 1–4 hour | Optional |
| Lead Time | 4–8 weeks | 6–10 weeks | 6–8 weeks | 4–8 weeks |
Fire-Rated & Hazardous Material Storage
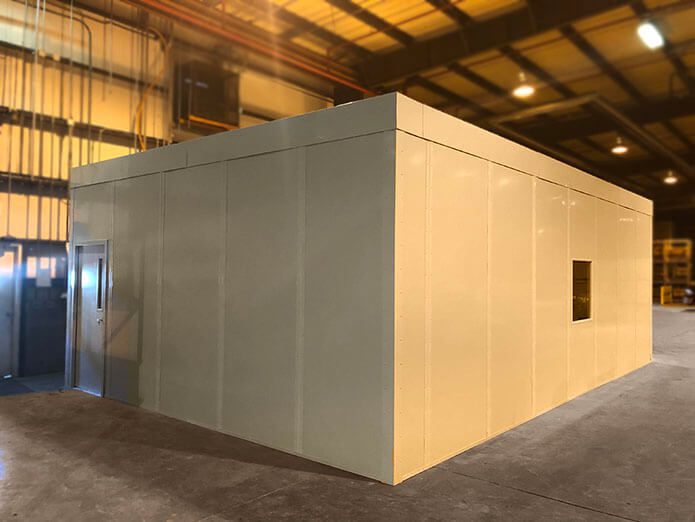
Our manufacturer partner builds UL-classified fire-rated modular walls and ceilings in 1-hour, 2-hour, and 4-hour ratings. These assemblies are tested and listed by Underwriters Laboratories and meet IBC requirements for fire-rated separations within industrial and commercial buildings. Common applications include flammable liquid storage rooms, lithium battery charging areas, paint mixing rooms, and code-required fire separations between hazardous and non-hazardous building zones.
Fire-rated modular construction offers significant advantages over conventional fire-rated construction. Traditional fire-rated walls require multiple layers of gypsum board, specialized framing, firestopping at every penetration, and extensive inspection. Modular fire-rated panels arrive pre-assembled, pre-tested, and UL-listed — eliminating the field assembly variability that can compromise fire ratings in conventional construction. Installation takes days instead of weeks, and the UL listing provides clear documentation for fire marshal approval.
Hazardous material storage rooms require specific ventilation, spill containment, electrical classification, and fire protection features in addition to fire-rated construction. Our manufacturer partner integrates explosion-proof lighting, mechanical exhaust ventilation, non-sparking hardware, and secondary containment sumps into fire-rated modular enclosures for facilities that store flammable, corrosive, or toxic materials. These turnkey solutions satisfy OSHA, EPA, and NFPA code requirements for hazardous material storage within occupied buildings.
For detached outdoor storage of drums, totes and flammables, see our guide to chemical and hazmat storage buildings: containment sumps, fire ratings, siting distances and ventilation.
Modular vs. Conventional Construction

The decision between modular and conventional construction comes down to four factors: speed, cost, flexibility, and tax treatment. Modular buildings are usually occupied sooner because factory fabrication happens concurrently with site preparation — there’s no weather delay, no subcontractor scheduling conflicts, and no field rework. A modular office that installs in days would take weeks with conventional drywall construction.
Total project cost often favors modular construction over stick-built equivalents. Factory efficiency eliminates the waste, rework, and coordination overhead inherent in field construction. Pricing set at drawing approval makes budgeting predictable — something conventional construction rarely achieves. Change orders, weather delays, and subcontractor conflicts routinely push conventional projects over their initial estimates.
Tax treatment is often the deciding factor for CFOs comparing options. Modular buildings classify as personal property (equipment) rather than real property (building improvements). This can allow 7-year MACRS accelerated depreciation versus 39-year straight-line depreciation for conventional construction — a significant cash-flow advantage in the early years of ownership. Section 179 expensing may also apply in some cases. Eligibility and treatment vary, so confirm with your tax advisor. Additionally, modular buildings are relocatable assets that move with your business rather than fixed improvements attached to a landlord’s property.
Industry Applications for Modular Buildings

Modular buildings serve virtually every industry because the fundamental value proposition — fast installation, lower cost, relocatable asset — applies universally. Manufacturing facilities use in-plant offices and quality inspection rooms built from modular panels to create controlled environments within production areas. The modular construction isolates office workers from manufacturing noise, dust, and temperature extremes while keeping management physically adjacent to production for rapid response to floor issues.
Distribution and logistics operations use modular buildings for shipping offices, driver check-in stations, returns processing areas, and battery charging rooms. The ability to relocate these structures as warehouse layouts evolve makes modular construction ideal for operations that reconfigure frequently — seasonal warehousing, e-commerce fulfillment, and third-party logistics facilities where client contracts change the required warehouse layout every 12–24 months.
Food and beverage processing facilities use modular cleanrooms and controlled-temperature rooms for packaging, quality testing, and product staging. Modular construction’s sealed panel system provides the sanitary, washable interior surfaces that USDA and FDA inspectors require. Agricultural operations use modular buildings for pesticide storage, equipment maintenance shops, and seasonal workforce housing. The portable nature of modular construction is particularly valuable for agricultural operations that expand and contract with growing seasons.
Government and military installations use modular buildings for temporary and semi-permanent facilities — command posts, training classrooms, equipment maintenance buildings, and secure storage rooms. GSA-approved modular building manufacturers satisfy federal procurement requirements and can deliver to military installations nationwide. The relocatable nature of modular construction is especially valuable for military installations that must rapidly deploy functional buildings to meet evolving mission requirements.
Ordering, Delivery & Relocation
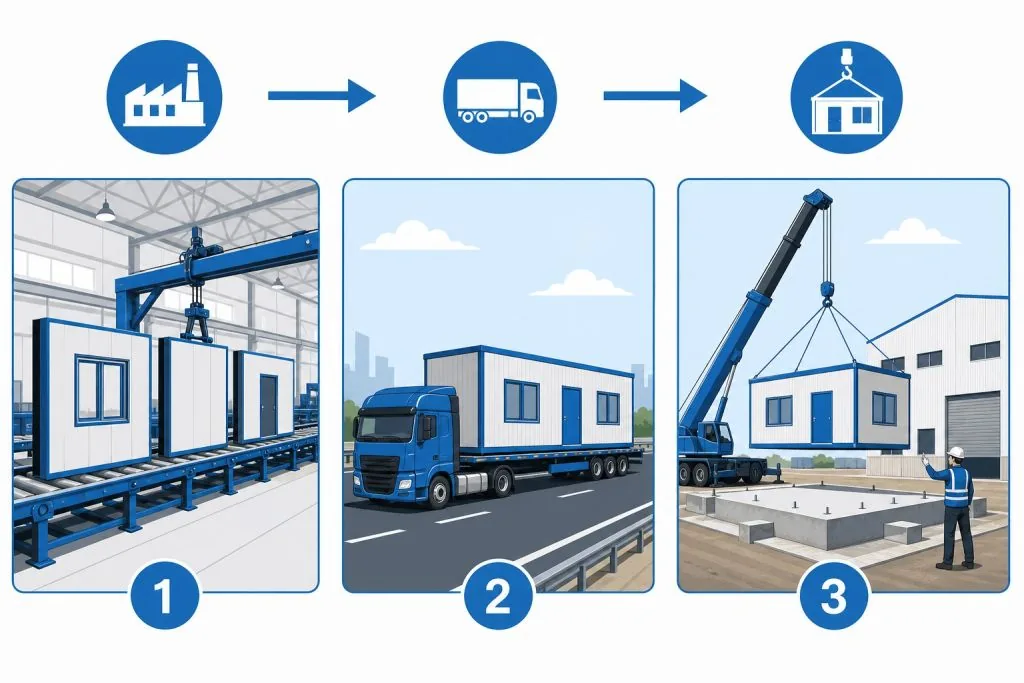
Our partner’s modular buildings are manufactured in its factory and shipped fully assembled or in large pre-finished sections to your site. Standard lead times range from 4–8 weeks for simple office configurations to 8–12 weeks for cleanrooms, fire-rated assemblies, and custom-engineered enclosures. Manufacturing happens in a controlled factory environment — no weather delays, no site disruption, and no coordination of multiple field subcontractors.
Delivery logistics depend on building size. Smaller buildings (up to approximately 12×40 feet) ship as complete assemblies on flatbed trailers and are crane-set onto prepared foundations in a single lift. Larger buildings ship as modular sections that are crane-set and bolted together on site — a process that typically takes 1–2 days for a multi-section building. Our manufacturer partner coordinates shipping logistics including route surveys, escort vehicles for oversize loads, and crane scheduling for the set day.
One of modular construction’s greatest advantages is relocatability. When your operation moves, expands, or reorganizes, modular buildings can be disassembled, transported, and reassembled at the new location. This preserves the capital investment in the building and its accelerated depreciation tax benefits. Our manufacturer partner designs every modular building for potential future relocation — connections are bolted (not welded), utility hookups are quick-disconnect, and panel systems are designed for repeated assembly and disassembly without damage or degradation.
Factory-built modular buildings are available through Material Handling USA with nationwide delivery and installation support. Whether you need a single-room supervisor office, a multi-room administrative suite, a controlled-environment cleanroom, or a fire-rated hazardous storage enclosure, our team specifies the right configuration for your application and manages the project from initial consultation through final inspection. Every modular building project includes detailed specifications, factory engineering drawings, delivery coordination, and installation oversight to ensure your building arrives on time and performs as specified from day one.
Modular Building vs Stick Build: Side-by-Side Comparison
The #1 question facility managers ask is whether to go modular or stick-built. Here’s how the two approaches compare across every factor that matters.
| Factor | Modular Building | Stick Build (Conventional) |
|---|---|---|
| Cost | Quoted per configuration (finished, installed); often lower total cost than conventional | Bid per project; higher labor, waste, and change-order exposure |
| Timeline | Often faster: 4–8 week lead time plus days on site. Factory work runs parallel to site prep. | Often months. Sequential trades, weather delays, and inspection holds add weeks. |
| Quality Control | Factory-controlled — consistent conditions, jigs & fixtures, multi-point QC | Variable — depends on crew skill, weather, and field supervision |
| Site Disruption | Minimal — 1–3 days of on-site assembly. Operations continue uninterrupted. | Months of noise, dust, contractors, and restricted access areas |
| Permits | Often simpler — classified as equipment/personal property in many jurisdictions | Full building permit process with multiple inspections required |
| Flexibility | Relocatable & expandable — panels disassemble and move to a new site | Permanent — demolition required for removal; expansion is a new project |
| Tax Treatment | 7-year MACRS depreciation; may qualify for Section 179 expensing (confirm with your tax advisor) | 39-year straight-line depreciation as real property improvement |
| Waste | Lower: factory cutting optimization reduces material waste | Higher field-cutting waste; dumpster and disposal costs add up |
| Resale Value | Retains value — can be sold and relocated as a used building asset | No separate resale — becomes part of the real estate (landlord’s asset) |
Bottom line: For warehouse offices, cleanrooms, guard houses, and equipment enclosures, modular construction delivers consistent factory-built quality, often at a lower total cost, with a shorter on-site schedule and far less disruption.
Why Modular Buildings Cost Less Than Stick-Built Construction
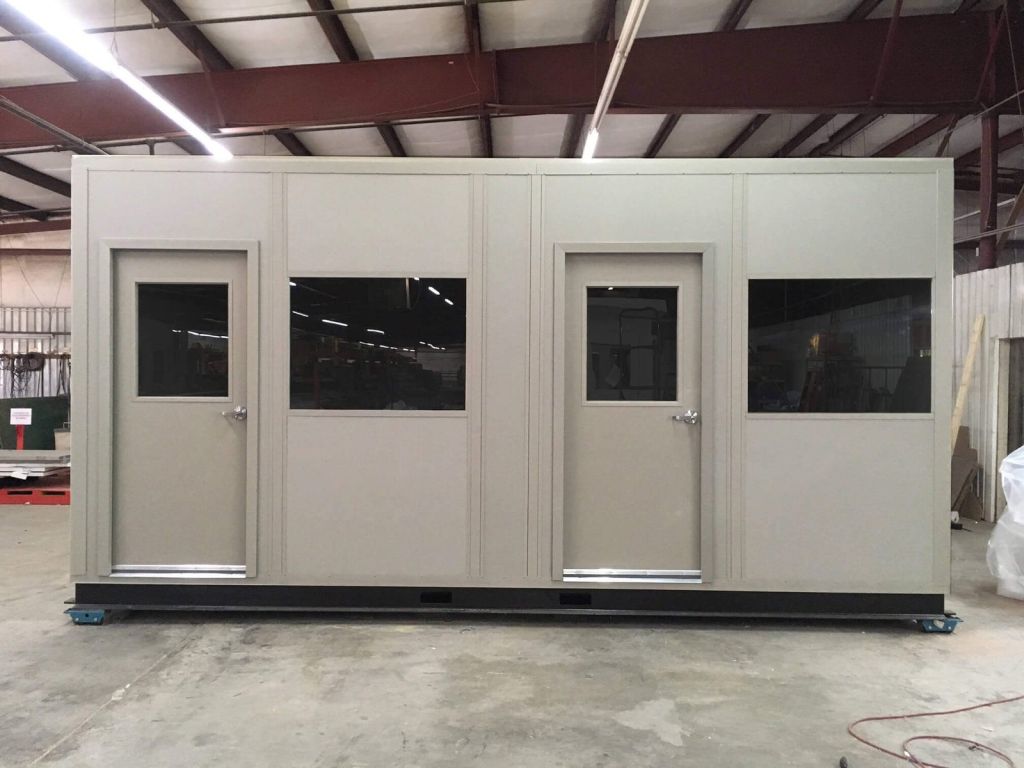
The cost advantage of modular construction isn’t about cutting corners — it’s about eliminating the inefficiencies inherent in field construction. Factory-built modular buildings often cost less in total than equivalent stick-built structures. Pricing depends on size, wall height, finishes, MEP (mechanical, electrical, plumbing) requirements and site conditions, so each building is quoted per configuration.
Here’s where the savings come from:
- Labor efficiency: Factory workers build in controlled conditions with specialized jigs and tools. No weather delays, no commute time, no waiting on other trades. Productivity is higher than in field construction.
- Less material waste: CNC cutting, pre-cut kits, and bulk purchasing reduce waste well below typical field construction. Materials are stored indoors — no weather damage or theft.
- No change-order surprises: Pricing is set when drawings are approved, so the price you are quoted is the price you pay for that scope. Conventional projects often run over budget due to change orders, weather delays, and subcontractor conflicts.
- Faster occupancy = faster ROI: When your building installs in days instead of months, you start using that space sooner, and those weeks of productivity count toward the return.
- Tax advantages multiply savings: Modular office buildings may qualify for 7-year MACRS accelerated depreciation and potential Section 179 expensing — versus 39-year depreciation for stick-built additions. Eligibility varies, so confirm the treatment with your tax advisor.
For budget planning, expect basic warehouse offices to cost less than offices with full MEP, and specialized cleanrooms or fire-rated enclosures to cost more. Pricing depends on size, wall height, options and site conditions, so request a free quote for your specific configuration.
How We Compare: Choosing the Right Modular Building Partner
The modular building industry includes several national manufacturers. Here’s what sets Material Handling USA apart when sourcing modular structures.
Multi-Vendor Access
Unlike buying direct from a single manufacturer, we source from top-tier factories to find the best fit for your specific project — whether that’s a simple 3-wall office or a multi-story cleanroom complex.
Competitive Pricing
We leverage dealer pricing from multiple manufacturers’ product lines. This means you get competitive bids without shopping multiple vendors yourself — we do the comparison for you.
Turnkey Project Management
From initial layout consultation through engineering, permitting, delivery coordination, and installation oversight, we manage every phase. You get a single point of contact instead of coordinating between manufacturer, freight, and installer.
Custom Engineering
Every project gets stamped structural engineering drawings from licensed PEs. We specify seismic loads, wind loads, snow loads, and fire ratings for your specific location — not generic catalog specs.
Full Product Range
Beyond modular buildings, we supply mezzanines, pallet rack, security cages, and complete warehouse design services. One vendor for your entire facility build-out.
Fast-Track Available
Emergency and fast-track projects are our specialty. Standard modular offices typically run on 4–8 week lead times. Rush projects using panels in stock at the manufacturer may ship sooner, subject to confirmation. Tell us your deadline and we’ll tell you what is possible.
Common Modular Building Applications by Industry
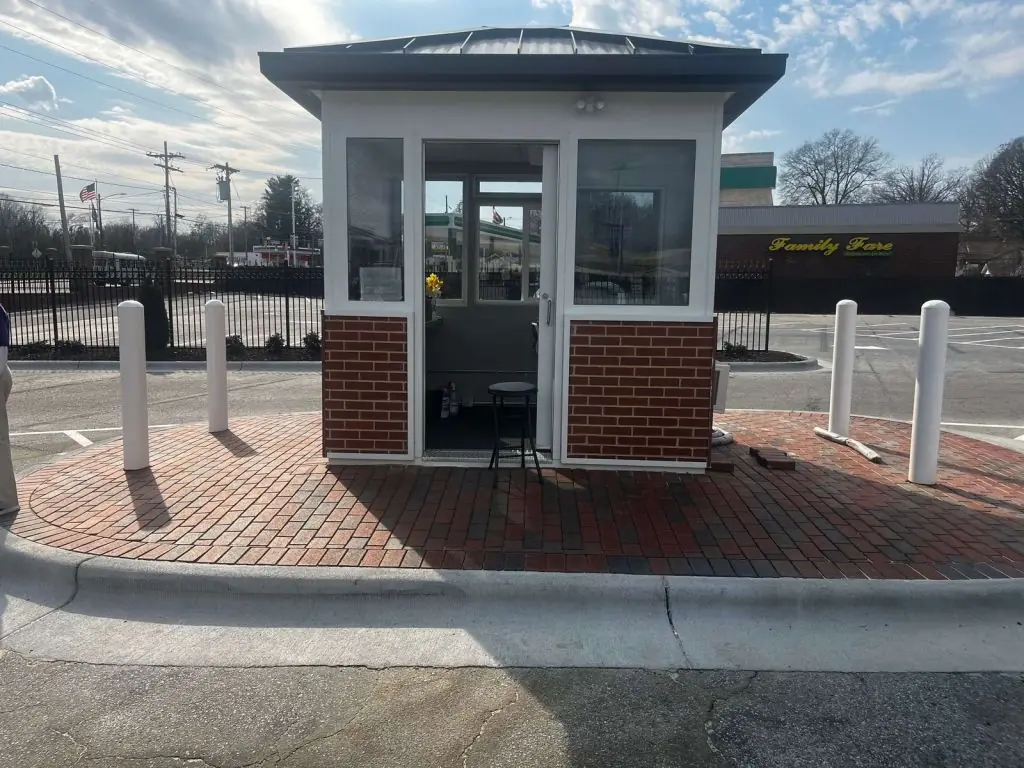
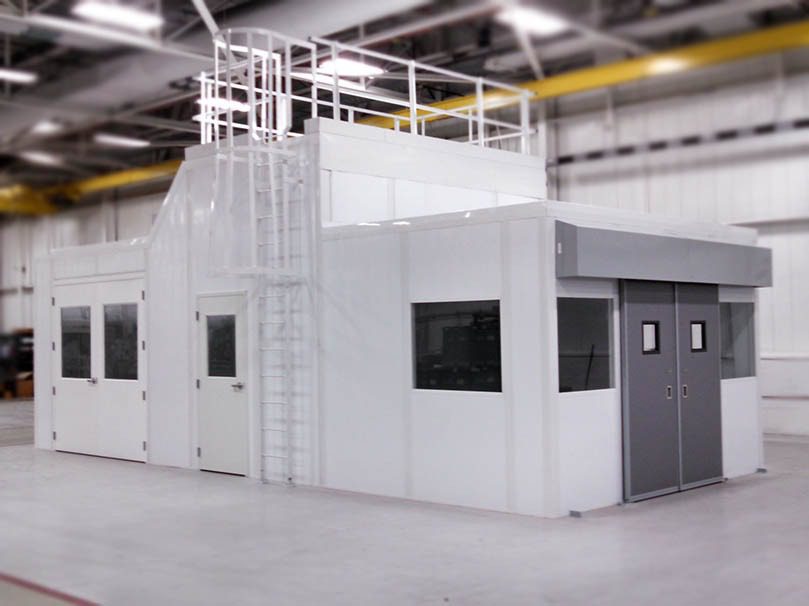
Modular construction serves nearly every industry. Here are the most common applications we design and install for customers across the Mountain West and nationwide.

Ready to Build Smarter?
Get a free modular building consultation with custom sizing, feature selection, and budget pricing. Our team responds within 24 hours.
Plan this before you buy
Free planning tools you can use right now — results on screen first, no gate to see them.
- Architect Specification Package BuilderAssemble the spec sections, data sheets and drawing references an architect needs to put storage and material handling into a bid set.
Industrial Modular Buildings
Industrial modular buildings are prefabricated, panel-built structures designed to be installed inside or alongside a working industrial facility — warehouses, manufacturing plants, distribution centres, maintenance garages, process plants and utility sites. They differ from commercial modular construction in three practical ways: they are built to survive an industrial environment, they have to be installed around an operation that cannot stop, and they are expected to be relocated when the facility layout changes.
The environment drives most of the specification. An office beside a press line is designed against radiant heat, impact noise and airborne particulate. An enclosure in a vehicle maintenance garage is designed around lift travel, crane paths and ventilation. A control room beside process equipment is designed for temperature stability and positive pressure. In every case the panel core, ceiling construction, glazing, door seals and mechanical package are selected against measured site conditions rather than a standard office package.
The installation constraint drives the rest. Panelized structures arrive flat-packed and bolt together on the existing slab with no wet trades, so a bay or aisle can usually be returned to service within days instead of the weeks a conventional build-out takes. The same bolted construction is what makes the structure relocatable later.
Industrial modular buildings are still buildings. Relocatable structures, including in-plant offices, are addressed by the International Building Code under Special Construction (Chapter 31) and otherwise have to meet the same applicable requirements as a site-built room of the same use and occupancy, so a permit is generally required even inside an existing facility. Egress, sprinkler coverage inside the new structure, fire alarm audibility and accessible routes are the items that most often need attention.
Common industrial applications:
- In-plant offices and supervisor stations — enclosed, conditioned space on the production floor with sightlines to the work.
- Quality control and metrology rooms — temperature-stable enclosures for CMMs, gauge labs and inspection benches.
- Maintenance and vehicle facility space — parts counters, diagnostics rooms and dispatch offices inside garages and shops.
- Equipment and sound enclosures — protecting machinery from the plant, or the plant from the machinery.
- Cleanrooms and controlled environments — filtered, pressure-controlled space built inside a conventional building shell.
- Modular break rooms, training rooms and welfare space — the highest acoustic and ventilation specification on the list.
Explore the applications above through the sections on this page, or tell us your site conditions and we will specify a structure against them.
Explore Modular Buildings by Location & Application
- Modular Buildings in Charlotte, NC
- Modular Buildings in Atlanta, GA
- Modular Buildings in Kansas City, MO
- Modular Buildings in Minneapolis, MN
- Modular Buildings in San Antonio, TX
- Modular Buildings in Dallas, TX
- Modular Buildings in Houston, TX
- Modular Buildings in Austin, TX
- Modular Buildings in San Diego, CA
- Modular Buildings in San Francisco, CA
- Modular Buildings in Los Angeles, CA
- Modular Buildings in Sacramento, CA
- Modular Buildings in Seattle, WA
- Modular Buildings in Portland, OR
- Modular Buildings in Phoenix, AZ
- Modular Buildings in Albuquerque, NM
- Modular Buildings in Nashville, TN
- Modular Buildings in Chicago, IL
- Modular Buildings for Automotive & Assembly Plants
- Custom Modular Building Solutions
- Modular Building Maintenance Guide
- Outdoor Smoking Shelters for Workplaces
- Modular Wall Systems & Warehouse Partition Walls
- Chemical & Hazmat Storage Buildings
- Lactation Pods
- Streaming Pods
- Cannabis Growing Facility Modular Solutions
- Modular Building vs Traditional Construction: The 2026 Guide
- Prefabricated Offices: Streamlining Your Workspace
- Modular Warehouse Office Cost Guide (2026)
- Top 7 Benefits of Modular Buildings for Modern Facilities
- Unpacking the Key Benefits of Modular Construction for Your Business